CO-NELEMixing & Granulation
Engineered for absolute slump uniformity, high volumetric output, and operational reliability in global infrastructure projects.
A Comprehensive Engineering Benchmark on Central Mix Batching Architecture, Fluid Dynamics, and Material Homogeneity Control.
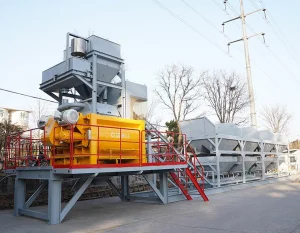
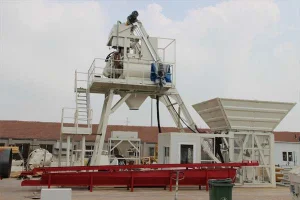
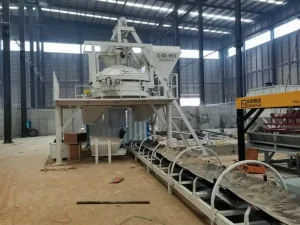
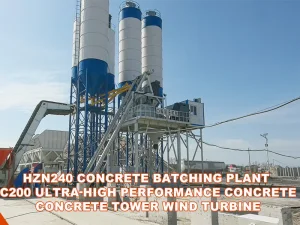
In modern industrial civil engineering, the transition from dry-batching (transit-mix) to centralized wet-mix concrete batching represents a quantum leap in concrete quality control, environmental sustainability, and chemical admixture efficiency. A Wet Mix Concrete Batching Plant (also designated as a Central Mix Plant) introduces a compulsory twin-shaft or vertical planetary mixer directly into the plant structure. Water, aggregates, cementitious materials, and liquid admixtures are fully homogenized prior to discharge into transit mixers or concrete pumps.
China's industrial engineering sector has established itself as the global epicenter for concrete machinery innovation. Operating from advanced manufacturing hubs in Qingdao and Shandong Province, manufacturers like CO-NELE leverage over two decades of metallurgical research, mechanical engineering patents, and automated production technologies. This whitepaper systematically evaluates the global industrial landscape, micro-structural mixing kinetics, smart control frameworks, and long-term economic dividends of sourcing premium wet mix batching infrastructure from leading Chinese factories.
Analyzing Macro-economic Demands, Decarbonization Mandates, and Regional Adoption Drivers.
Driven by strict EN 206 and ASTM C94 standards, infrastructure contractors demand zero-slump consistency and precise air-entrainment control. Low-carbon concrete recipes involving high volumes of fly ash, slag (GGBS), and silica fume necessitate intensive compulsory shear mixing that dry-mix plants cannot deliver.
Extreme ambient temperatures require wet mix plants equipped with integrated chilled water dosing, flake-ice batching systems, and high-speed cement cooling jackets to prevent flash setting and maintain initial slump workability during mega-project pours.
Rapid urban migration and massive high-speed railway networks create immense demand for modular, high-capacity ready-mix batching plants (120 m³/h to 180 m³/h) capable of 24/7 continuous operation with minimal wear-and-tear downtime.
Mechanical Kinematics, High-Chrome Alloy Metallurgy, and High-Precision Transducer Systems.
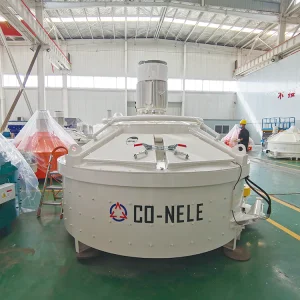
The core heart of a wet mix concrete batching plant is its mixer unit. Chinese engineering has advanced two distinct compulsory mixing paradigms to perfection:
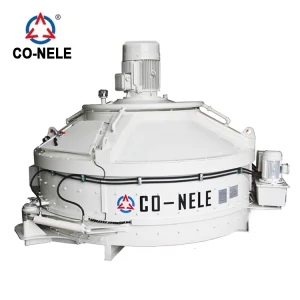
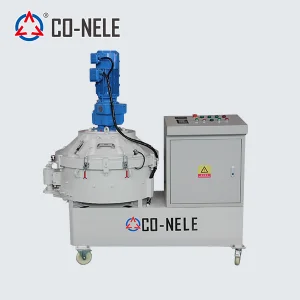
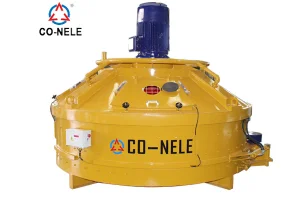
Vertical-Shaft Planetary Counter-Current Mixers: Utilizing dual or triple mixing star arms that rotate on their own axes while revolving around a central point. This creates complex 3D turbulence paths within the pan, preventing material segregation and guaranteeing 99.9% dispersion of micro-silica, color pigments, and synthetic fibers within 30 to 45 seconds of mixing cycle time.
Horizontal Twin-Shaft Compulsory Mixers: Designed for high-volumetric infrastructure applications (HZS90, HZS120, HZS180 plants). Dual counter-rotating shafts equipped with streamlined spiral mixing blades force materials into cross-directional shear vortexes, maximizing mechanical energy transfer while reducing energy consumption per cubic meter by up to 15%.
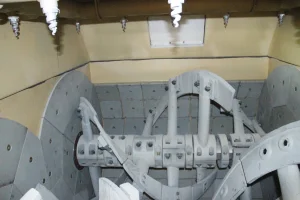
A primary bottleneck in heavy-duty concrete production is liner and blade abrasion. Advanced Chinese manufacturers utilize proprietary Ni-Hard and High-Chrome Cast Iron alloys (HBW ≥ 600 hardness rating) for mixing tiles and paddle tips. In-house engineered planetary gearboxes feature forged alloy steel gear teeth, vacuum-carburized heat treatment, and multi-stage oil seal protection to withstand torque shocks up to 45,000 N·m without thermal distortion.
Achieving structural concrete compliance mandates razor-thin dosing tolerances. Wet mix plants incorporate multi-point strain gauge load cells with 24-bit digital signal conversion processing:
Pioneering the Transition Toward Autonomous, Cloud-Monitored, and Zero-Carbon Concrete Production.
Fully automated batching control with real-time recipe management, cloud reporting, remote fault diagnostics, and predictive maintenance alerts via IoT sensors.
Continuous in-mixer electrical resistance and microwave moisture sensing, automatically compensating added water per batch to preserve exact target slump.
100% recycling of truck washout slurry water and un-hardened aggregate back into active production, achieving zero-water-discharge environmental certification.
Gaseous CO2 dosing into wet mix mixing chambers, mineralizing carbon dioxide into nano-calcium carbonate particles to boost concrete compressive strength by 10-15% while sequestering carbon.
Tailored Machinery Configurations for Specialized Downstream Sector Demands.
Requires hyper-consistent color and zero surface bug-holes. Paired with planetary mixers (CMP series), wet mix plants supply ultra-homogeneous mixes for architectural cladding, hollow-core slabs, structural columns, and precast utility vaults.
Ultra-High-Performance Concrete (UHPC) exhibits extreme viscosity and high steel fiber loading. CO-NELE specialized UHPC batching plants integrate reinforced drives and high-shear rotors to achieve >150 MPa compressive strength specifications.
Large-volume dam mass concrete demands low-heat hydration cement mixes with large maximum aggregate sizes (up to 120 mm). Heavy-duty twin shaft wet plants (CHS series) ensure continuous, rapid batching cycles without stone jamming.
De-risking International Procurement Through Strict Manufacturing Standards and On-the-Ground Engineering Support.
Procuring capital industrial machinery internationally requires complete confidence in electrical compliance, structural safety standards, and long-term spare parts availability. Chinese manufacturers have established rigorous global support frameworks:
All wet mix batching plants strictly conform to CE Machinery Directive 2006/42/EC, ISO 9001:2015 quality management systems, EAC (Eurasian Conformity), and optional UL/CSA electrical control panel standards for North American deployment.
Equipped with dual-frequency, wide-voltage drive motors (220V to 480V, 50Hz/60Hz), Schneider/ABB switchgear, and multi-language PLC software interfaces (English, Spanish, Russian, French, Arabic).
Standardized, bolt-on wear liner tiles, mixer paddle blades, pneumatic valves, and load cell components are stocked in regional hubs, guaranteed to dispatch within 24 to 48 hours to minimize plant downtime.
Expert Guidance Addressed by Senior Technical Directors to Help You Make Informed Plant Equipment Decisions.
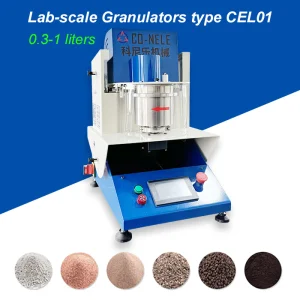
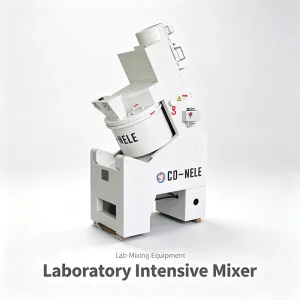
Explore our complete portfolio of advanced concrete mixers, intensive granulators, and custom precast plants.