CO-NELEMixing & Granulation
Global demand for concrete has shifted radically from standard residential grades to high-durability, structural-grade formulations. Major transport corridors, deep-water port infrastructure, high-speed rail networks, and offshore wind turbines demand precise water-cement ratios and consistent micro-dispersion that older tilting-drum mixers simply cannot achieve.
Modern Ready Mix Concrete (RMC) production increasingly incorporates SCMs (Supplementary Cementitious Materials) such as pulverized fly ash (PFA), ground granulated blast-furnace slag (GGBS), and silica fume. Integrating micro-powders into dense recipes requires intense shear energy to prevent agglomeration and ensure complete hydration.
Chinese ready mix concrete plants for sale have evolved from low-cost alternatives into global benchmarks for mechanical reliability and industrial automation. Leveraging vertically integrated metallurgical supply chains, advanced CNC machining center fabrication, and robust PLC automation, Chinese factories supply equipment operating across 80+ countries.
| Performance Metric | Vertical Planetary Counter-Current Mixer | Horizontal Twin-Shaft Compulsory Mixer | Traditional Tilting-Drum Mixer |
|---|---|---|---|
| Primary Application | Precast, UHPC, GFRC, High-Spec Block & Pavers | High-Volume Commercial Ready Mix, Dam Construction | Low-Grade Site Mix, Non-Structural Work |
| Mixing Homogeneity (CV) | < 3% (Micro-level uniformity) | < 5% (Standard structural grade) | > 12% (High variance risk) |
| Fiber & Pigment Dispersion | Superior (Eliminates micro-balling completely) | Moderate (Requires extended batching cycles) | Poor (Severe segregation occurs) |
| Discharge Velocity | Rapid via bottom hydraulic sweeping gate | Ultra-rapid dual-door opening | Slow gravity tilt process |
| Wear Life (High-Chrome Alloys) | 120,000 – 160,000 batches | 80,000 – 110,000 batches | 15,000 – 30,000 batches |
Multi-compartment storage hoppers equipped with electro-pneumatic discharge gates and high-precision strain-gauge load cells. Real-time dynamic weighing algorithms compensate for aggregate falling head impact, guaranteeing batch accuracies within ±1.0% for aggregates and ±0.5% for cementitious powders.
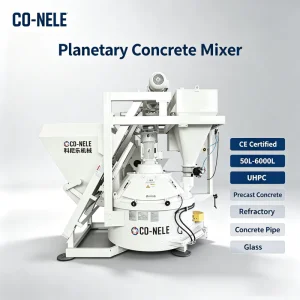
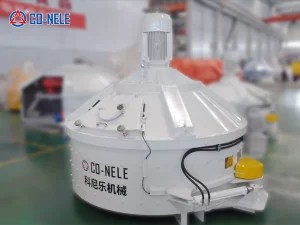
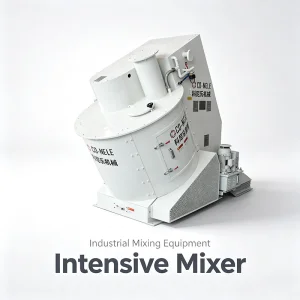
The transmission is the heart of any vertical planetary mixer. Factory-engineered heavy-duty planetary speed reducers transmit dual-rotation kinematics: mixing arms rotate around the central axis while simultaneously spinning on their own axes. This complex planetary trajectory leaves zero dead angles in the mixing pan.
High-frequency microwave moisture probes integrated into the discharge gate or pan floor measure real-time aggregate moisture levels 25 times per second. The PLC automatically adjusts water dosing online to maintain targeted water-cement ($w/c$) ratio and slump consistency.
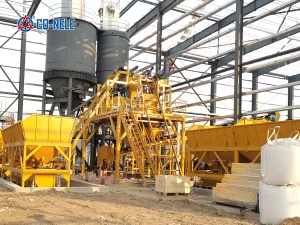
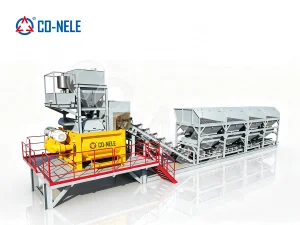
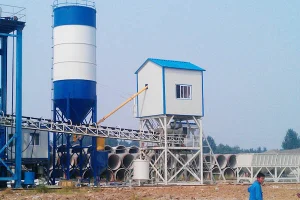
For high-capacity commercial ready-mix plants producing 90 $m^3/h$ to 240 $m^3/h$, our stationary HZS series plants feature fully enclosed aggregate storage towers, active pulse dust collectors, dual cement weigh hoppers, and automated vehicle dispatch software integration to maximize hourly throughput.
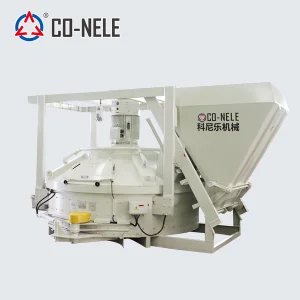
Precast component fabrication (architectural panels, bridge girders, prestressed hollow-core slabs, concrete pipes) demands consistent moisture and color uniformity. Planetary concrete mixers configured with skip hoists deliver high-strength concrete with rapid discharge cycles directly to molding machines.
UHPC manufacturing requires severe shear force to disperse steel micro-fibers, silica fume, and fine quartz flour. Our specialized high-intensive mixers utilize high-speed rotor impellers capable of handling low water-binder ratios ($w/b < 0.18$) without overheating or motor stall.
Designed for rapid mobilization in road construction, dam building, and remote mining sites. Our foundationless concrete batch plants eliminate massive concrete civil foundations, allowing total setup within 72 hours on compacted ground using steel base plates.
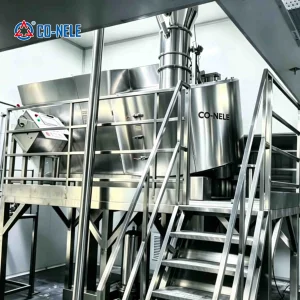
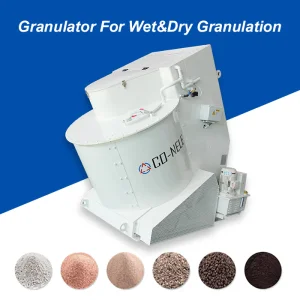
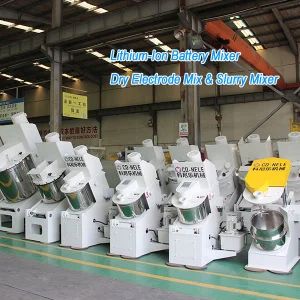
Beyond traditional construction concrete, intensive mixers and granulating equipment serve high-value industrial sectors including refractory castables, ceramic powders, battery cathode paste, diamond abrasives, and fertilizer pelletizing with pinpoint binder addition.
Engineered for global environmental extremes: fully insulated winterized enclosures with steam heating jackets for Siberian winter projects (down to -35°C), alongside heavy-duty ice-water batching and liquid nitrogen cooling systems for tropical Middle Eastern ambient conditions (+50°C).
All structural steelwork, pressure vessels, and mechanical systems are built to European standards. Electrical cabinets strictly observe IEC 60204-1 and CE Directives, featuring Schneider electric components, dual-channel emergency stop safety relays, and interlocking maintenance hatch switches.
For US and Canadian deployments, batching controls adhere to ASTM C94 / C94M specification for ready-mixed concrete. Control systems utilize NEMA-rated enclosure panels with UL/CSA listed breakers, Allen-Bradley PLCs, and imperial calibration readouts.
Custom electrical drive engineering accommodates local site supply requirements worldwide: 220V/380V/415V/440V/480V at 50 Hz or 60 Hz frequencies. High-efficiency VFDs (Variable Frequency Drives) smooth motor start-ups and reduce peak grid demand penalties.
Integration of cloud-connected vibration sensors and thermal imaging to predict gearbox bearing wear 500 operating hours prior to component failure.
In-pan optical slump sensors dynamically fine-tuning chemical admixture dosing during active mixing, eliminating manual slump tests entirely.
Complete integration of wastewater recycling, greywater clarification systems, aggregate reclamation, and rooftop solar power compatibility.
Full-autonomy concrete production: autonomous aggregate loader feeding combined with AI-driven dispatching without human site presence.
Choose a vertical-shaft planetary counter-current mixer when producing high-specification mixes (UHPC, GFRC, color paving blocks, precast concrete, refractory castables) where micro-homogeneity below a 3% Coefficient of Variation is mandatory. Choose a twin-shaft compulsory mixer for high-volume commercial ready-mix plants (above 90 m³/h output) where cycle speed (30–45 seconds per batch) and high batch volumes take priority.
Under standard aggregate abrasion conditions, our high-chromium alloy wear liners (hardness > 65 HRC) typically achieve 120,000 to 150,000 batch cycles. For highly abrasive applications such as quartz powder or dense refractory castables, liner life ranges between 40,000 and 60,000 batches. All wear elements are modular, bolt-on, and easily replaceable during routine maintenance shutdowns.
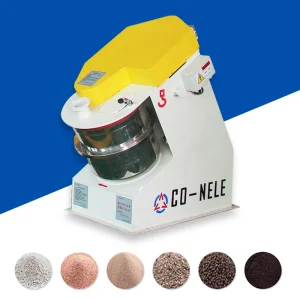
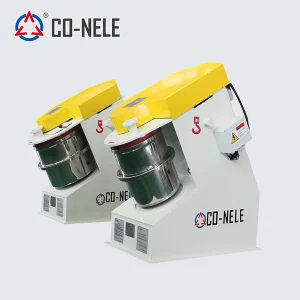
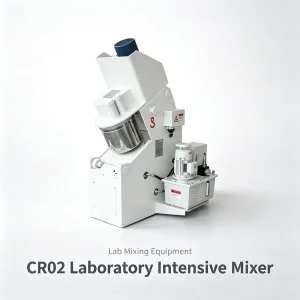
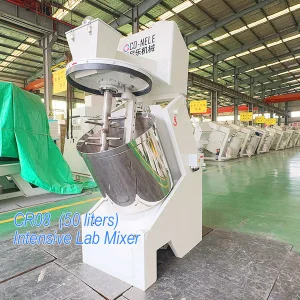
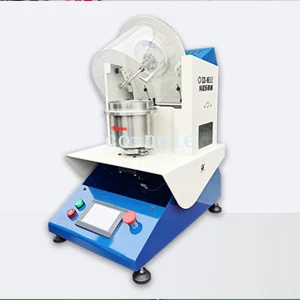
Yes. Our Qingdao process testing laboratory maintains lab-scale intensive mixers and planetary units from 5 to 75 liters. Clients can send 10 to 50 kg of raw materials (powders, aggregates, binders) for benchmark testing. We provide detailed empirical test reports covering granule sphericity, density, mix homogeneity, and scale-up parameters.
Plants are engineered in modular sub-assemblies formatted for 40ft High Cube (40HC) container transport or flat rack containers. Every order includes foundation layouts, schematic electrical diagrams, and step-by-step assembly guides. We provide remote video commissioning supervision as well as resident field service engineers for on-site erection and crew training.
All machines come standard with a 12-month structural and drive gear warranty. We stock standardized replacement parts (wear liners, mixing arms, pneumatic valves, load cell sensors, planetary gears) in our Qingdao logistics hub for express international air shipment within 24 to 48 hours of request.