CO-NELEMixing & Granulation
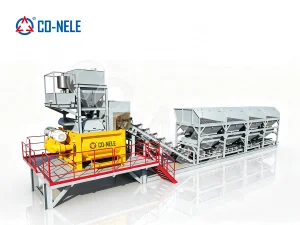
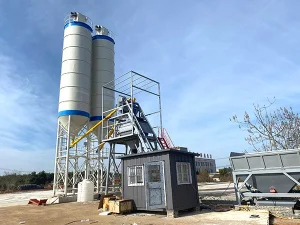
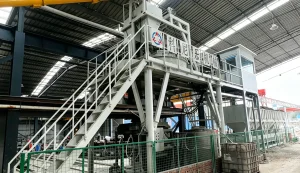
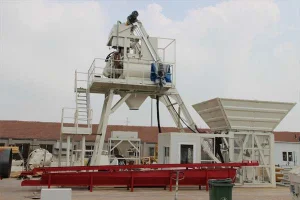
The China HZS90 Concrete Batching Plant represents a pivotal threshold in medium-to-large scale industrial concrete manufacturing. Designed for high-intensity commercial ready-mix (RMC) production, highway bridge engineering, dam construction, and precast element manufacturing, the HZS90 plant seamlessly bridges the gap between compact mobile units and massive double-station stationary complexes. Yielding a theoretical capacity of 90 cubic meters per hour, this system is engineered around a forced dual-horizontal-shaft compulsory mixer (typically the JS1500 twin-shaft model) paired with a high-precision PLD2400 aggregate batching machine.
In modern concrete engineering, achieving optimal slump consistency, structural integrity, and durability demands rigorous control over material micro-homogeneity. The HZS90 integrates heavy-duty structural steelwork with advanced automation technology, utilizing dynamic multi-stage aggregate dosing, high-resolution load cells, and digital pneumatic control. By optimizing shear stress distribution within the mixing trough, the plant minimizes cement consumption while maintaining structural strength parameters that comply with ISO, ASTM, DIN, and GB/T international concrete standards.
| Technical Parameter | HZS90 Engineering Specification | Operational Impact & Benefit |
|---|---|---|
| Theoretical Capacity | 90 m³/h (1.5 m³ per batch cycle) | Maximizes output throughput for large fleet ready-mix dispatching. |
| Main Mixer Unit | JS1500 Compulsory Twin-Shaft (1.5m³ discharge) | Rapid shearing force achieves micro-homogeneity in 30–45 seconds. |
| Aggregate Dosing Bin | PLD2400 (4 Bins, 4 x 25m³ capacity) | Supports multi-grade gravel and sand aggregate storage simultaneously. |
| Weighing Accuracy | Aggregates ±2%, Cement/Fly Ash ±1%, Water ±1%, Additive ±1% | Eliminates material yield variation and lowers costly binder consumption. |
| Aggregate Max Diameter | 60 mm (Crushed Stone) / 80 mm (Pebble Gravel) | Accommodates heavy civil engineering aggregate recipe requirements. |
| Discharge Height | 3.8 meters – 4.2 meters (Standard RMC Truck Clearance) | Seamlessly feeds standard 8m³–12m³ transit mixer trucks. |
| Total Installed Power | ~145 kW to 175 kW (Depending on Silo Configurations) | High energy efficiency ratio (kWh/m³) optimized by soft-start drives. |
| Control Architecture | Fully Automatic Siemens PLC + Industrial PC SCADA System | Provides real-time cloud data logging, recipe memory, and auto-dosing calibration. |
A deep structural analysis of the China HZS90 Concrete Batching Plant reveals an integrated ecosystem where mechanical power, material dynamics, and digital controls function in synchronized harmony. Each sub-system is stress-tested using Finite Element Analysis (FEA) to endure 24/7 continuous duty cycles in high-abrasion, dust-heavy environments.
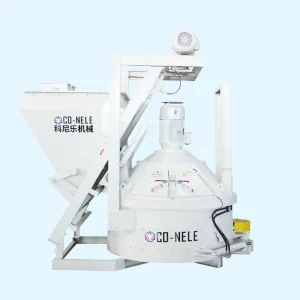
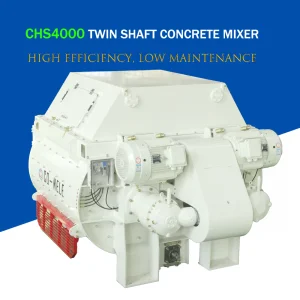
At the heart of the HZS90 is the JS1500 twin-shaft compulsory mixer. Dual horizontal shafts rotate counter-directionally at optimized RPMs, forcing spatial movement of aggregate particles across 3D counter-current paths.
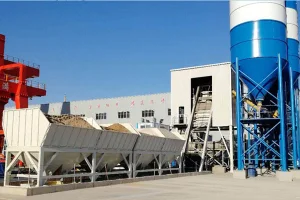
The aggregate batcher features a 4-compartment storage hopper handling fine sand, coarse sand, medium gravel, and large crushed stone.
Cement, fly ash, slag powder, water, and chemical admixtures are independently weighed in suspended hoppers positioned directly above the mixer.
The global dominance of Chinese machinery manufacturing in the concrete mixing sector is rooted in advanced Industry 4.0 automation, complete vertical integration, and resilient supply chain infrastructure. China’s leading HZS90 concrete batching plant factories are no longer merely assembling bought-in components—they operate fully integrated smart manufacturing ecosystems.
From heavy-plate structural steel framing to precision gear machining, top-tier Chinese manufacturers employ 6-axis robotic arc welding cells, large-format CNC gantry milling machines, and laser-cutting tables. Structural weld joints undergo ultrasonic non-destructive testing (NDT), ensuring that support towers, mixer chassis, and aggregate bins endure earthquake loads, extreme wind stress, and thermal expansion cycles.
Leading factories house their own metallurgical foundries, formulating custom wear alloys for mixing arms, wear plates, and planetary gearboxes. By executing complete drive-train load testing—where every JS1500 mixer gear reducer undergoes continuous bench testing under 120% nominal load—factories guarantee zero out-of-box component failure upon overseas delivery.
The versatility of the HZS90 plant makes it an ideal workhorse across diverse global industrial application scenarios. Below is a breakdown of how specialized configurations solve specific engineering requirements:
Transport infrastructure projects demand rigid slump consistency, low water-cement ratios, and continuous high-volume concrete discharge.
Solution Configuration: The HZS90 is equipped with dynamic microwave moisture sensors integrated into aggregate bins, automatically adjusting water metering in real-time. Paired with twin 100-ton cement silos and fly ash dosing, the plant produces C50–C80 high-strength concrete capable of meeting stringent bridge pier and tunnel lining specifications.
Commercial concrete suppliers require fast formula switching, dual transit truck loading lanes, and comprehensive environmental protection.
Solution Configuration: HZS90 plants feature fully enclosed tower structures with integrated pulse-jet dust collectors installed at every material transfer point. The SCADA system stores over 100 distinct concrete mix designs, allowing dispatchers to switch from standard residential pump concrete to colored architectural mix with a click of a button.
Precast operations (wall panels, culverts, prestressed beams, concrete poles) require ultra-precise batch sizing and dry-cast zero-slump capability.
Solution Configuration: The HZS90 plant can be customized with a planetary counter-current mixer option or enhanced JS1500 speed control drives, synchronizing directly with automated overhead concrete distribution buckets and mold casting systems.
Harbor construction requires marine-grade anti-corrosion concrete enriched with silica fume, blast-furnace slag, and anti-washout chemical additives.
Solution Configuration: Multi-powder silo connections (up to 4 silos) with specialized powder micro-dosing systems and heavy-duty stainless steel liquid additive scales ensure chemical resistance against marine sulfate attack.
As global climate goals drive decarbonization and digitalization in construction, Chinese concrete machinery engineering is undergoing a transformative technological transition. The next decade of HZS90 plant iterations will focus on three key pillars:
Future HZS90 systems incorporate artificial intelligence neural networks connected to mixer motor current sensors and optical camera sensors inside the mixing pan. By analyzing real-time electrical torque feedback and fluid dynamics, the AI dynamically measures micro-rheology and adjusts mixing time, superplasticizer dosage, and water ratio mid-batch.
Next-generation HZS90 green batching plants feature closed-loop water treatment and aggregate reclaiming systems. Concrete truck washings are automatically separated into stone, sand, and gray slurry water. The recycled slurry water is monitored for specific gravity and re-injected into non-structural concrete mixes, eliminating liquid effluent waste.
With Ultra-High Performance Concrete (UHPC) gaining rapid adoption in bridge deck overlays and defense works, standard HZS90 plants are evolving modular upgrade kits. These include high-shear planetary mixing heads, automated steel-fiber dosing units, and temperature-controlled steam/ice dosing systems for extreme climate casting.
When procurement directors and engineering executives evaluate purchasing an HZS90 concrete batching plant from China, analyzing total cost of ownership (TCO) yields a clear strategic advantage over local European or American equivalents.
A high-specification Chinese HZS90 plant delivers equivalent output and automation quality at 40%–60% lower initial capital cost than traditional Western brands. This capital savings can be reallocated to larger mixer truck fleets or aggregate storage infrastructure.
Equipped with IE3 high-efficiency motors, variable frequency drives (VFD), and optimized batch cycle management, the HZS90 reduces electrical power consumption per cubic meter of concrete mixed to under 1.4 kWh/m³.
Standardized high-chrome wear blades and liners reduce maintenance downtime. Fast-wearing components are engineered for quick 4-bolt field replacement, minimizing plant downtime to under 2 hours per maintenance cycle.
Based on a standard single-shift operating model producing 450 m³/day, most commercial ready-mix operators amortize their initial HZS90 plant investment within 6 to 9 months of active site operations.
Cross-border machinery procurement requires absolute assurance regarding electrical compatibility, safety regulations, and environmental standards. Leading Chinese batching plant manufacturers implement localized manufacturing options tailored to target export regions:
Electrical control cabinets are built to regional power specifications: 220V/380V/415V/440V/480V at 50Hz or 60Hz. Wiring systems utilize standardized Schneider, Siemens, and ABB electrical switchgear with UL / CE certification marks.
Machines are fully compliant with EU Machinery Directive 2006/42/EC, CE standards, and OSHA safety guidelines. Safety interlocks on mixer inspection hatches prevent motor startup when service personnel are inside.
Supported by resident commissioning engineers and cloud-based Remote Telematics. Overseas plant operators can grant secure remote access to factory engineers for diagnostic software troubleshooting and PLC calibration.
Explore our broader spectrum of forced-action mixing systems, intensive granulators, mobile batching plants, and ultra-high-performance concrete solutions.
Below are explicit engineering answers to common technical queries raised by global project managers and machinery purchasers regarding the HZS90 concrete batching plant: