
CO-NELEMixing & Granulation
Engineered to meet rigorous California environmental standards, seismic zone requirements, and high-spec mix designs.
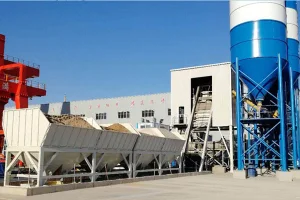
Counter-current mixing technology engineered for zero-segregation SCC and high-strength commercial mixes in Bay Area urban projects.
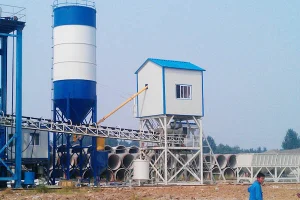
Heavy-duty automated batching system optimized for zero-slump dry-cast concrete used in California civil drainage works.
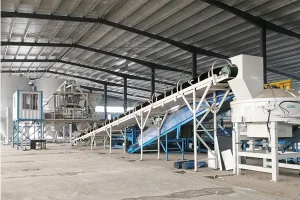
Precision color-consistency and rapid-batching plant configured for tilt-up panels and architectural precast facades.
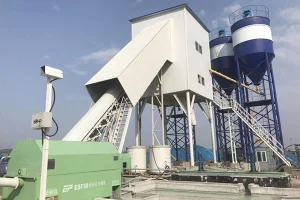
High-throughput 90 m³/h commercial plant with integrated dust extraction compliant with BAAQMD clean air guidelines.
Navigating California's Strict Building Standards, Low-Carbon Mandates, and High-Density Urban Infrastructure Demands
The San Francisco Bay Area represents one of the most technologically advanced and environmentally regulated construction markets in North America. Driven by large-scale infrastructure investments—including the California High-Speed Rail corridor, San Francisco International Airport (SFO) modernization, transbay transit enhancements, and resilient seismic retrofitting—the demand for high-performance concrete (HPC) and ultra-high-performance concrete (UHPC) has reached unprecedented levels.
Operating a concrete batching plant in Northern California, however, presents unique engineering and operational challenges. Batching operations must comply strictly with Caltrans Section 90 specifications, Bay Area Air Quality Management District (BAAQMD) Regulation 6 Rule 1 (dust and particulate control), and California Assembly Bill 2446 regarding embodied carbon reduction in building materials.
As a leading Chinese concrete batching plant manufacturer, CO-NELE integrates cutting-edge planetary mixing technology, UL-certified automation, and modular environmental enclosures to empower Bay Area concrete producers with maximum yield, batch precision, and compliance security.
Advanced Kinematics Designed for Micro-Homogeneity and Rapid Batching Cycles
CO-NELE vertical-shaft planetary mixers rotate on a complex counter-current star trajectory. This guarantees 100% material coverage without dead zones, releasing trapped cement clusters and dispersing color pigments evenly in under 45 seconds.
For high-volume commercial ready-mix concrete above 2 m³ per batch, our CHS twin-shaft compulsory mixers utilize dual hydraulic discharge gates, continuous spiral mixing arms, and floating shaft seal protection to resist high abrasive friction.
All aggregate bins, mixer support towers, and cement silo structures exported to the San Francisco market undergo finite element analysis (FEA) to withstand severe California earthquake forces and wind gusts up to 110 mph.
| Engineering Metric | Planetary Batching Plant (CMP) | Twin-Shaft Batching Plant (CHS) |
|---|---|---|
| Primary Application | Precast, UHPC, GFRC, Block & Pipe, Colored Concrete | High-Output Commercial Ready-Mix, Mass Infrastructure |
| Mixing Homogeneity (CV) | < 3% (Ultra-Micro Uniformity) | < 5% (Standard Commercial Uniformity) |
| Mixing Cycle Time | 45 – 60 Seconds | 30 – 45 Seconds |
| Wear Liner Service Life | 120,000+ Batches (Rhombus High-Chrome) | 90,000+ Batches (Ni-Hard / Hardox) |
| Dry-Cast / Zero Slump Mixes | Exceptional Efficiency | Moderate Performance |
Integrating Artificial Intelligence, Real-Time Rheology Sensors, and Carbon Mineralization into San Francisco Operations
Equipped with high-frequency microwave moisture sensors inside aggregate bins and the mixing pan, our intelligent control system adjusts added water dynamically per millisecond to compensate for sand moisture variations.
To support Silicon Valley and SF carbon neutrality mandates, CO-NELE batching plants feature modular carbon-dioxide injection ports directly into the planetary mixing chamber, permanently sequestering recycled $\text{CO}_2$ into nano-calcium carbonate matrixes.
Zero-discharge environmental recycling systems collect truck washouts and mixer rinsing water, separating aggregate via sand-washers and re-dosing slurry water using real-time specific gravity sensors.
Ensuring Seamless Permitting, Fast Commissioning, and Continuous Operation across the Bay Area
Electrical safety is non-negotiable in California. CO-NELE delivers fully certified UL-508A control cabinets equipped with Siemens or Allen-Bradley PLCs, Schneider main circuit breakers, and industrial touchscreens, guaranteeing smooth local building inspection approvals in San Francisco and San Jose.
Safety features include heavy-duty mechanical safety interlocks on mixer inspection doors, emergency stop buttons situated at every operator workstation, non-slip elevated walkway catwalks, and full drive-belt protective covers designed to satisfy Cal/OSHA workplace safety inspectors.
To eliminate fugitive cement dust in urban SF job sites, our aggregate batchers, belt conveyors, and cement silos feature dust-tight seals, high-efficiency pulse-jet baghouse collectors, and pressure-relief safety valves with automatic alerts.
With direct ocean freight routes into the Port of Oakland, equipment delivery lead times are optimized. Critical wear components—such as mixer liner plates, mixing blades, pneumatic valves, and load cells—are maintained for rapid dispatch.
Why CO-NELE’s 30,000 m² Qingdao Production Base Delivers Unmatched Precision and Value
CO-NELE (Qingdao CO-NELE Machinery Co., Ltd.) established in 2004, holds over 80 national patents and participated in drafting China's national mixing equipment industry standards. Operating 3 advanced production bases, we manufacture planetary gearboxes, heavy steel frames, and mixing pans in-house.
Contact Engineering TeamUnlike assembly-only suppliers who purchase third-party gearboxes, CO-NELE designs and machines its own heavy-duty planetary reducers. This in-house capability guarantees that speed ratios, gear hardness, and torque ratings are optimized specifically for severe concrete mixing friction.
Precision CNC laser cutting ensures air-tight aggregate bin joints and perfectly aligned drive shafts.
Every planetary gearbox undergoes 24-hour continuous load test bench trials before factory shipment.
SEW-EURODRIVE motors, Hardox wear liners, WAM dust collectors, and Toledo load cells integrated seamlessly.
Delivering premium European-grade mixing performance at 40-50% lower total capital investment.
Explore Mobile, Stationary, Compact, and Precast Plants Built for High ROI and Operational Reliability
Compact 35 m³/h precast plant optimized for localized block, curbing, and architectural element manufacturing.
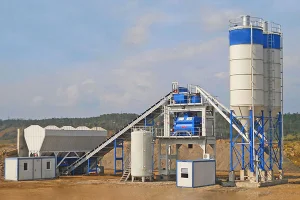
Heavy-duty 90 m³/h output with skip-hoist or inclined belt conveyor designed for continuous commercial delivery.
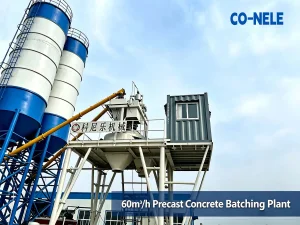
Featuring a CMP1000 planetary mixer core, delivering rapid batching cycles for high-specification precast slabs.
Flagship 180 m³/h mega-plant engineered for major highway paving, transit tunnels, and high-rise foundations.
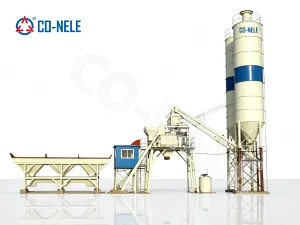
Optimized small-footprint modular layout designed specifically for confined San Francisco urban job sites.
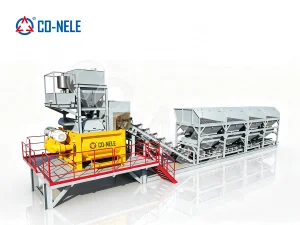
Eliminates expensive concrete foundation work; installs directly on compacted soil in under 3 days.
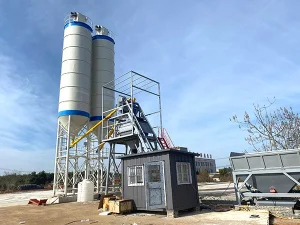
Highly mobile trailer-mounted batching unit ideal for remote bridge repair and quick-response utility contracts.
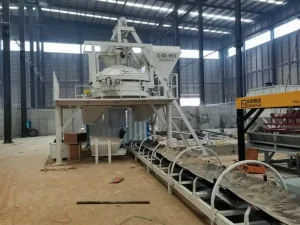
Dedicated high-precision batching line designed for structural wall panels and insulated concrete forms (ICF).
Expert Answers Prepared by Senior CO-NELE Application & Process Engineers
Contact our application engineering team today to receive custom plant layout drawings, technical engineering proposals, and a competitive factory-direct quote.
Send Inquiry Now