
CO-NELEMixing & Granulation
Understanding why the 60 m³/h capacity benchmark represents the strategic operational sweet-spot for global infrastructure, ready-mix suppliers, and precast manufacturers.
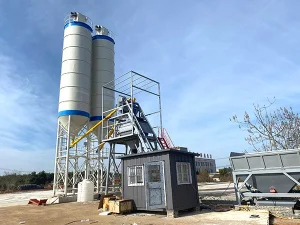
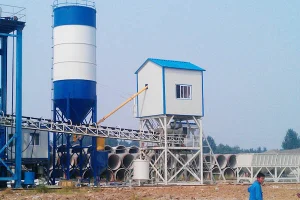
The HZS60 Concrete Batching Plant stands as the single most versatile production unit in industrial civil engineering. Delivering a nominal throughput of 60 cubic meters of compacted concrete per hour, it strikes an optimal equilibrium between capital expenditure (CAPEX), footprint efficiency, and high-duty operational output.
In rapidly urbanizing corridors across Southeast Asia, the Middle East, Latin America, and Africa, HZS60 plants serve as the foundational bedrock for commercial ready-mix operations and highway construction. Chinese engineering manufacturers, led by innovation pioneers like CO-NELE, have redefined global supply chains by exporting high-reliability, PLC-automated HZS60 configurations built to international ISO and CE standards.
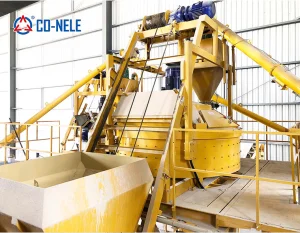
Featuring a 1.0 m³ batch discharge cycle (JS1000 twin-shaft or CMP1000 planetary mixer), an HZS60 complete plant maximizes mixer motor efficiency while maintaining a swift 60-second aggregate-to-discharge loop. This yields unprecedented return on investment (ROI) with payback periods frequently achieved within 8 to 14 months of continuous site operations.
A deep breakdown of core sub-systems engineered by Qingdao CO-NELE Machinery Co., Ltd.
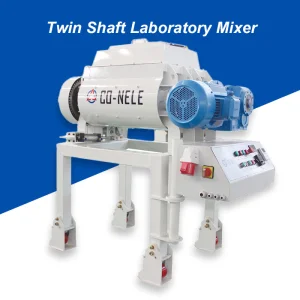
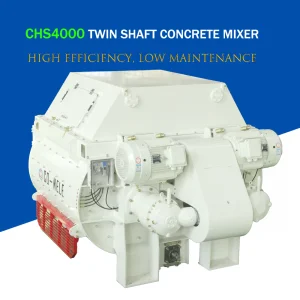
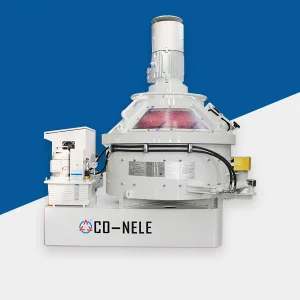
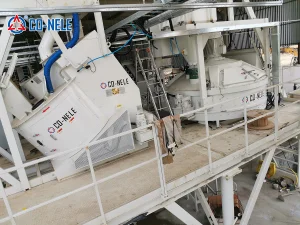
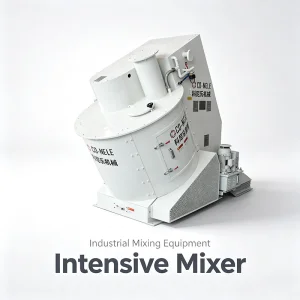
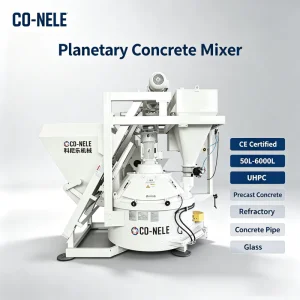
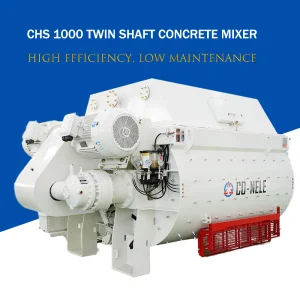
The operational core of the HZS60 plant centers around its forced mixer unit. While traditional ready-mix suppliers opt for the CHS Series Twin Shaft Mixer (1.0m³ output) for rapid mass concrete discharge, high-spec precast, UHPC, and paving brick manufacturers integrate the CMP Counter-Current Planetary Mixer.
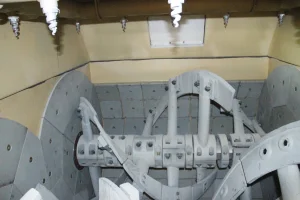
The counter-current vertical planetary action eliminates mixing dead zones, driving aggregate dispersion at a molecular level with a Coefficient of Variation (CV) under 5%, vital for high-strength C60+ formulations.
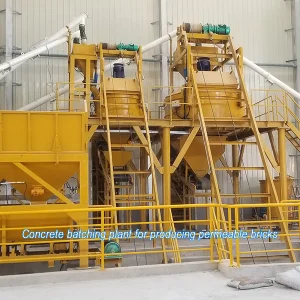
The HZS60 utilizes the PLD1600 Aggregate Batcher, configured with 3 to 5 independent storage bins (sand, fine gravel, coarse stone). Equipped with load-cell sensors under the hopper, aggregates are weighed cumulatively or independently.
Material transport to the mixer overhead bin is executed via a heavy-duty skip hoist or an inclined corrugated sidewall belt conveyor, reducing footprint requirements without sacrificing material velocity.
Quality concrete requires unyielding precision. Cement, fly ash, and mineral powders are metered through dedicated suspension hopper scales equipped with pneumatic butterfly valves and high-sensitivity tension sensors (precision ±1%).
Water dosing features a pressurized spray bar system for fast distribution into the pan, while chemical admixtures are metered through stainless steel liquid-loss weighers with dynamic recipe adjustment capabilities.
Operating through a Siemens-based PLC interface, the HZS60 provides full-auto, semi-auto, and manual control modes. The software manages real-time aggregate moisture compensation, cloud-connected batch logging, automatic error correction, and downloadable delivery receipts.
| Specification Parameter | HZS60 Standard (Skip Hoist) | HZS60 Heavy-Duty (Belt Conveyor) | HZS60 Precast Specialty (Planetary) |
|---|---|---|---|
| Theoretical Productivity | 60 m³/h | 60 m³/h | 50 - 60 m³/h |
| Main Mixer Unit | JS1000 Twin-Shaft (1000L) | CHS1000 Twin-Shaft (1000L) | CMP1000 Planetary Mixer (1000L) |
| Aggregate Batching Model | PLD1600 (3-4 Bins) | PLD1600 (4-5 Bins) | PLD1600 High-Precision Dosing |
| Discharge Height | 3.8m / 4.0m | 4.0m / 4.2m | Customized / Track System |
| Weighing Accuracy | Agg: ±2%, Powder: ±1%, Water: ±1% | Agg: ±1.5%, Powder: ±0.5%, Water: ±0.5% | Agg: ±1%, Micro-dosing: ±0.2% |
| Total Installed Power | ~110 kW | ~125 kW | ~135 kW |
How China's leading batching plant manufacturers are driving sustainable, automated, and carbon-neutral concrete production.
Modern HZS60 engineering now embeds digital carbon footprint calculators into the batching controller. By supporting supplementary cementitious materials (SCMs) like slag, ground limestone, and silica fume, plants achieve up to a 40% reduction in embodied carbon per batch.
Integrating microwave moisture probes directly within aggregate discharge gates and inside mixer pans allows real-time dynamic water compensation. The system calculates water-cement ratios automatically prior to discharge, guaranteeing consistent concrete slump.
Leading Chinese factories incorporate closed-loop sand-gravel re reclaimers and sludge water recycling agitators into HZS60 layouts. Advanced pulse-jet fabric filter collectors installed on cement silos maintain airborne dust emission below 10 mg/Nm³.
Engineering tailored HZS60 plant configurations to solve complex construction site challenges worldwide.
Challenge: Precast products (interlocking pavers, culverts, prestressed beams, wall panels) require dry-cast or zero-slump concrete with uniform pigment distribution and flawless surface finish.
CO-NELE HZS60 Solution: An HZS60 plant equipped with a CMP1000 Planetary Concrete Mixer, flying bucket overhead delivery track, and multiple additive dosing channels. Eliminates pigment streaks, guarantees fast cycle times, and interfaces directly with block machinery.
Challenge: Remote road construction sites demand rapid setup, heavy-duty durability against harsh ambient conditions, and continuous high-output operations without unexpected downtime.
CO-NELE HZS60 Solution: A modular, Foundationless Mobile/Compact HZS60 Configuration. Steel foundation pads replace deep concrete foundations, allowing commissioning within 4 days. Includes heavy-duty wear liners and dual-gate rapid discharge.
Challenge: High-density urban environments require strict noise abatement, minimal dust emissions, and rapid truck mixer loading cycles.
CO-NELE HZS60 Solution: Fully enclosed steel-structure housing for the main mixing tower and aggregate bins, integrated soundproof insulation, automated truck positioning sensors, and high-capacity pneumatically-operated cement batchers.
Challenge: UHPC formulations demand high shear energy to disperse micro-silica fume powders and steel fibers without clumping.
CO-NELE HZS60 Solution: Customized HZS60 featuring an upgraded high-torque planetary gearbox, variable frequency speed control (VFD), and hardened ceramic alloy mixing blades designed to handle dense, high-viscosity shear loads.
Two decades of dedicated mixing machinery engineering, 80+ patents, and direct factory manufacturing.
Unlike assemblers who buy third-party reduction gearboxes, CO-NELE designs and machines proprietary vertical planetary gearboxes in our own 30,000 m² Qingdao facility, guaranteeing rigorous quality control and direct spare-part availability for decades.
CO-NELE participated directly in drafting national mixing machinery standards in China. Holding over 80 granted patents, our engineering authority is recognized across refractories, precast concrete, glass, and powder metallurgy industries globally.
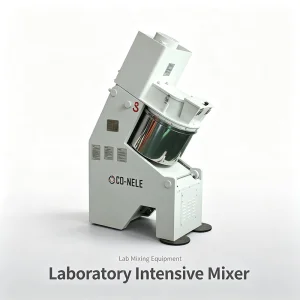
Before issuing equipment proposals, our Qingdao lab conducts raw material mixing and trial granulations (from 5L to 75L scales) to benchmark aggregate shear, binder consumption, bulk density, and required cycle times for your exact recipe.
Pioneering the intelligent, autonomous batching plants of tomorrow.
Integration of vibration, temperature, and wear sensors inside gearboxes and mixer bearings, transmitting live diagnostics to plant managers to eliminate unpredicted downtime.
AI neural networks automatically adjusting water-cement-admixture ratios in real-time based on ambient humidity, aggregate moisture, and raw material batch variations.
Full integration with solar-storage microgrids, electric truck charging infrastructure, and total closed-loop greywater/aggregate re-utilization modules.
Adaptive planetary mixing arm velocity profiles that dynamically adjust RPM based on torque feedback, optimized for bio-based and ultra-low-carbon geopolymer mixes.
Expert technical answers to assist global buyers, engineers, and plant operators.
A standard skip-hoist HZS60 plant requires an operational footprint of approximately 22m × 15m (330 m²), excluding cement storage silos and aggregate storage yards. If selecting an inclined belt conveyor layout for high-throughput commercial ready-mix, the length extends to roughly 45m × 15m (675 m²). Modular foundationless options reduce civil construction preparation area by up to 30%.
Choose a vertical-shaft CMP Planetary Counter-Current Mixer when your production calls for dry-cast concrete, pigmented paving blocks, precast structural elements, GFRC, or UHPC, where mixing homogeneity must achieve a Coefficient of Variation (CV) below 5%. Choose a CHS Twin Shaft Mixer for conventional commercial ready-mix or high-volume wet concrete above C30, where rapid 30-45 second cycle times take priority over micro-homogeneity.
All CO-NELE equipment is custom-engineered to match local global industrial power grids, including 220V, 380V, 415V, 440V, 480V at 50Hz or 60Hz. Electrical cabinets feature premium Schneider, ABB, or Siemens switchgear and can be built to full CE-compliance standards.
Manufactured from high-chrome alloy casting (hardness ≥62 HRC), standard liners and blades run between 90,000 to 150,000 batch cycles under normal aggregate concrete production, and 40,000 to 60,000 cycles under highly abrasive refractory or quartz sand UHPC conditions. All wear parts are bolt-on for fast field replacement, with spare parts stocked in Qingdao for immediate worldwide dispatch.
Yes. CO-NELE operates an advanced process laboratory in Qingdao with lab mixers from 5 to 75 liters. Overseas customers can ship 10–20 kg of raw powder/aggregate samples to test mixing homogeneity, binder ratio requirements, granule sphericity, and bulk density. Our process engineers deliver a detailed test report to guide equipment selection.
Contact CO-NELE’s engineering design office today. Send your material characteristics, target daily capacity, and site layout for a complete technical proposal and factory-direct quotation.