CO-NELEMixing & Granulation
Explore CO-NELE's high-precision equipment lineup engineered for ultra-homogeneity, heavy-duty durability, and custom plant integration.
Modern construction ecosystems demand rigorous material consistency, zero-carbon footprint efficiency, and automated formulation scaling. China's dry mix batching plant manufacturing sector has evolved from mechanical assembly to advanced process engineering.
The global transition from traditional job-site wet mixing to centralized factory dry-mix batching is accelerating. Major drivers include stringent urban dust regulations, strict quality controls for structural renders and tile adhesives, and the explosive growth of Ultra-High Performance Concrete (UHPC) and self-leveling compounds. Dry mix factories require continuous, dust-free dosing systems capable of homogeneously blending fine powders down to micro-silica scales.
Established in 2004 in Qingdao, Shandong, Qingdao CO-NELE Machinery Co., Ltd. stands at the forefront of compulsory mixing innovation. Operating 3 state-of-the-art production bases spanning 30,000 m², CO-NELE integrates proprietary planetary gearbox design, heavy wear-plate metallurgy, and smart PLC automation, serving over 10,000 industrial users in 80+ countries.
International EPC contractors, commercial ready-mix operators, and building material conglomerates evaluate dry mix batching plants on critical metrics that dictate operational profitability and lifecycle total cost of ownership (TCO).
The Coefficient of Variation (CV) measures batch uniformity. Premium dry mix mortars (such as tile adhesives, micro-silica grouts, and thermal insulation renders) require CV < 3%. CO-NELE planetary and intensive counter-current mixers achieve complete micro-dispersion within 60 to 90 seconds, avoiding additive agglomeration.
Raw material costs are heavily influenced by chemical additives (cellulose ethers, redispersible polymer powders, accelerators). Global buyers demand aggregate dosing accuracy within ±1.0% and micro-ingredient dosing precision within ±0.2% via loss-in-weight screw feeders.
Processing quartz sand, crushed granite, and abrasive minerals rapidly erodes mixing pan liners. Enterprise buyers demand bolt-on, interchangeable high-chrome alloy liners (HB600+ hardness) and ceramic-coated mixing blades that deliver 120,000+ batch lifetimes before replacement.
Procurement Insight: China-manufactured batching plants provide up to 40% CapEx savings compared to Western European alternatives without compromising on component quality. CO-NELE standardizes on Siemens PLCs, Schneider electrics, Hardox/High-Chrome liners, and Bonfiglioli/proprietary heavy gearboxes.
Different dry mortar recipes and concrete grades dictate specific mixing physics and structural plant configurations. Understanding these technical dynamics ensures optimal machine selection.
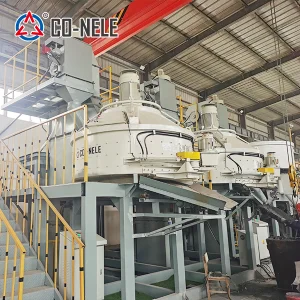
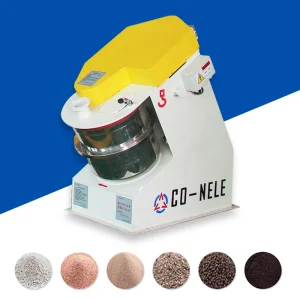
The mixing star and blades rotate around a central axis while simultaneously orbiting the entire pan circumference. This dual-rotation movement creates intensive shear forces and continuous cross-current turnover without centrifugal segregation. It is the gold standard for dry-cast concrete, UHPC, refractory castables, and pigmented dry mortars.
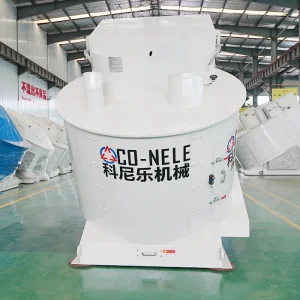
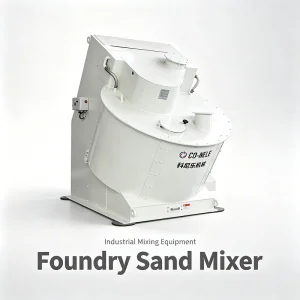
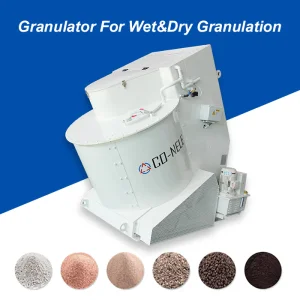
Combining an inclined rotating pan with a counter-rotating high-speed rotor tool, this technology generates fluidization and high mechanical energy. Ideal for chemical powder granulation, ceramic powders, diamond abrasives, and fine dry mortar coating applications where micro-granule sphericity (90%+) is required.
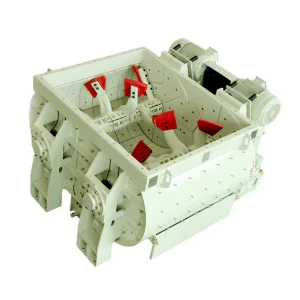
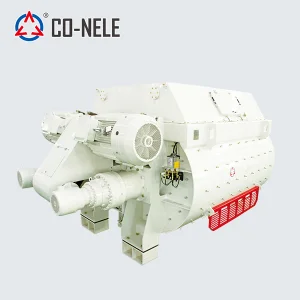
Featuring counter-rotating double shafts with synchronized paddle placement, twin-shaft mixers create a 3D fluidization zone. Designed for high-volume ready-mix batching plants (180 m³/h capacity) where rapid cycle times (30–45 seconds) and fast hydraulic gate discharge are mandatory.
Specifically built for dry mortar formulations containing light aggregates (e.g., expanded perlite, EPS granules). The gentle yet thorough double-spiral ribbon action ensures zero breakdown of fragile lightweight aggregates while achieving complete pigment dispersion.
| Plant Layout Concept | Target Throughput | Footprint & Height | Dosing Accuracy | Best Suited Application |
|---|---|---|---|---|
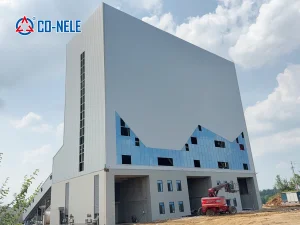
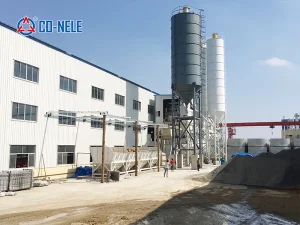
| Tower-Type Dry Mix Plant | 30 – 120 Tons/Hour | Compact Footprint, Height 24m–38m | ± 0.5% (Gravity Flow) | High-capacity urban dry mortar, tile adhesive, self-leveling factories. |
| Stepped / Two-Stage Plant | 15 – 60 Tons/Hour | Medium Footprint, Height 12m–18m | ± 1.0% (Bucket Conveyance) | Commercial mortar manufacturers, medium-scale regional suppliers. |
| Horizontal / Compact Line | 5 – 25 Tons/Hour | Large Floor Area, Height 6m–9m | ± 1.0% (Screw Conveyance) | Specialty chemical mortars, insulation mortars, small footprint operations. |
| Mobile Towable Batching Unit | 25 – 50 m³/h / 20 T/h | Trailer-Mounted, Zero Foundation | ± 1.5% (Integrated PLC) | Remote infrastructure projects, highway bridge joints, on-site UHPC. |
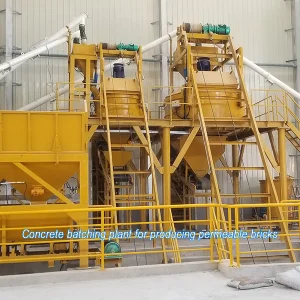
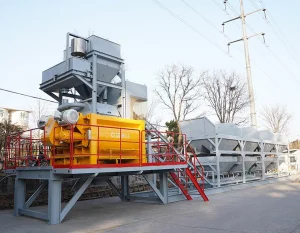
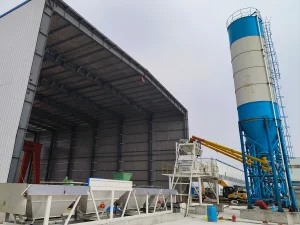
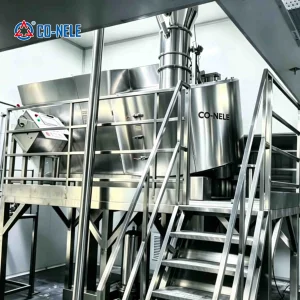
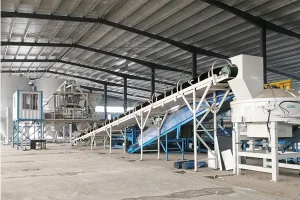
A turnkey China dry mix batching plant integrates raw material processing, screening, thermal drying, precision dosing, compulsory mixing, and automated packaging.
Raw river sand or crushed stone is passed through a triple-pass rotary dryer to drop moisture below 0.5%. Multi-deck vibrating screens classify aggregate into specific fractions (e.g., 0-0.6mm, 0.6-1.2mm, 1.2-2.5mm) stored in dedicated silos.
Cement, fly ash, slag powder, and limestone fillers are stored in sealed steel silos equipped with pneumatic fluidization cones and dust collectors. Weigh hoppers mounted on high-precision load cells batch materials sequentially.
The CO-NELE compulsory mixer receives weighed components and minor additives. After a 60-second homogeneous mix cycle, material drops into a surge hopper feeding automatic impeller or pneumatic valve-bag packing machines and bulk truck loaders.
The next decade will transform concrete and dry mortar production. CO-NELE is actively pioneering smart sensor integration and low-emission equipment architectures.
Integrating microwave moisture sensors and real-time drive-motor torque monitoring into the mixing pan allows the control system to dynamically adjust water/admixture dosing during the active batch cycle. This guarantees identical workability despite raw aggregate moisture fluctuations.
As the construction industry adopts Calcined Clay Limestone Cement (LC3), alkali-activated geopolymers, and industrial by-product binders, dry mix mixers must process sticky, fine-particle recipes. CO-NELE high-shear planetary mixers eliminate balling and agglomeration inherent to low-clinker formulations.
IoT vibration and temperature sensors installed directly on gearbox bearings feed telemetry data to a central cloud dashboard. Maintenance teams receive automated alerts before mechanical failure occurs, ensuring near-zero unplanned plant downtime.
Modern dry mix plants handling organic additives, starch ethers, and aluminum powder require full ATEX explosion protection. CO-NELE equips mixing vessels with negative-pressure air circulation, pulse-jet filter units, and explosion-venting valves.
Delivering mixing machinery worldwide requires strict compliance with regional electrical codes, structural standards, and fast localized spare-parts availability.
All CO-NELE export machinery is CE-certified, complying with Machinery Directive 2006/42/EC and Low Voltage Directive 2014/35/EU. Structural steel towers comply with EN 1090 standards for seismic and wind load durability.
Panels are built to client specification: 220V/380V/415V/440V/480V at 50Hz or 60Hz. Standard integration includes Siemens S7 PLCs, touchscreens, and Schneider low-voltage components for easy local sourcing.
CO-NELE maintains a comprehensive inventory of interchangeable planetary wear arms, high-chrome liner plates, and gearbox seal kits. Guaranteed dispatch within 24-48 hours ensures minimal plant disruption.
Answers curated by CO-NELE process application engineers to guide equipment evaluation and plant layout design.
Explore additional specialized machinery from CO-NELE, engineered for ready-mix, ceramic powders, pipe production, and laboratory testing.