
CO-NELEMixing & Granulation
High-efficiency mixing units engineered for rapid cycle times, high aggregate shearing, and rigorous compliance with US Department of Transportation (DOT) standards.
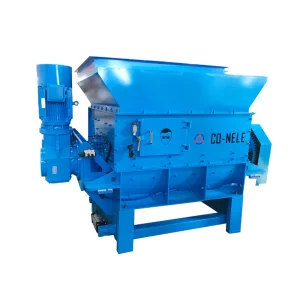
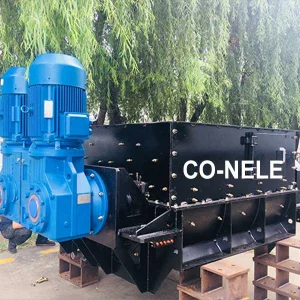
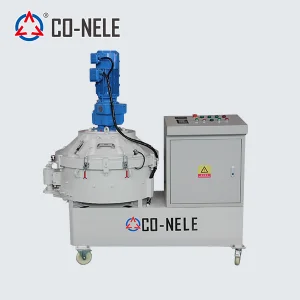
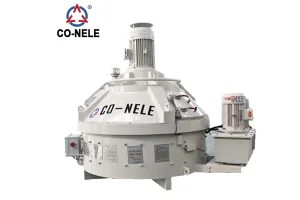
The United States operates the world's most extensive road transportation network, encompassing over 4 million miles of paved public roads and interstates. Driven by the federal funding commitments under the Infrastructure Investment and Jobs Act (IIJA), state Departments of Transportation (DOTs) across North America are executing unprecedented highway rehabilitation, airport runway upgrades, and urban paving projects.
Achieving the long-term durability demanded by federal and state standards (such as AASHTO M323 and Superpave mix specifications) hinges on a single critical factor: absolute homogenisation of liquid bitumen, aggregate fractions, mineral fillers, and recycled asphalt pavement (RAP). Conventional continuous drum mixers often struggle to maintain tight mix tolerances during short batch changes or high-percentage RAP incorporation. This operational bottleneck has catalyzed a nationwide shift toward high-throughput, forced-action Twin Shaft Asphalt Mixers.
In asphalt paving, thermal segregation and bitumen binder stripping are the primary causes of premature rutting and fatigue cracking. Twin shaft compulsory mixers eliminate micro-segregation by imparting intense synchronized counter-rotating three-dimensional spatial turbulence, ensuring every aggregate particle is thoroughly coated with a uniform liquid asphalt film within a compressed 30-to-45 second mixing window.
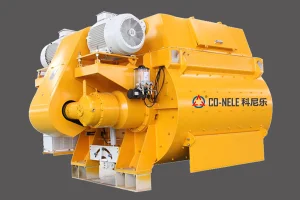
Unlike free-fall tilting drum mixers or single-shaft pugmills, the twin shaft compulsory mixer utilizes two horizontal counter-rotating shafts equipped with synchronized mixing arms and overlapping paddle geometry. This creates a highly turbulent fluidised zone where aggregate collision energy accelerates binder dispersion.
Overlapping paddle paths force materials to cycle axially and radially simultaneously. This fluidised mixing movement reduces friction heat loss while achieving complete binder encapsulation in seconds.
Engineered to handle high proportions of Reclaimed Asphalt Pavement (up to 50%+ RAP) without binder breakdown, preventing thermal degradation of virgin bitumen and reducing virgin oil consumption.
Pan liners and mixing paddles are cast from ultra-durable High-Chromium alloy (Cr26) with hardness exceeding 62 HRC, standing up to abrasive quartzite and crushed granite aggregates.
| Performance Parameter | CO-NELE Heavy Duty Twin Shaft | Traditional Single Shaft Pugmill | Continuous Drum Mixer |
|---|---|---|---|
| Mixing Cycle Time | 25 – 45 seconds | 60 – 90 seconds | Continuous (Variable) |
| Co-efficient of Variation (CV) | < 3.0% (Ultra-homogeneous) | < 7.5% | < 10.0% |
| Max RAP Incorporation | 50% – 65% (With WMA Dosing) | 20% – 30% | 30% – 40% |
| Wear Parts Service Life | 120,000 – 150,000 Batches | 50,000 – 70,000 Batches | Medium / High Scour |
| Bitumen Coating Uniformity | 99.8% Particle Encapsulation | 94.5% Particle Encapsulation | 91.0% Particle Encapsulation |
| US Electrical Compliance | NEMA 4X / UL 508A Certified | Standard Custom | Varies by OEM |
Climatic variations across North America—from the freezing freeze-thaw cycles of the Midwest and Northeast to the searing heat of the Southwest deserts—demand highly localized asphalt mix recipes. CO-NELE Twin Shaft Asphalt Mixers are custom-engineered to meet these specific regional challenges:
Designed for continuous batch production of dense-graded Superpave hot-mix asphalt (HMA) and stone matrix asphalt (SMA). Ensures zero aggregate degradation during mixing to satisfy strict state DOT smoothness and rut-resistance metrics.
Heavy airfield pavement demands rigorous compliance with Federal Aviation Administration FAA P-401 standards. Our mixers deliver flawless dispersion of polymer-modified binders (PMA) and heavy additives required to resist jet-fuel and heavy aircraft loads.
Integrated water-foaming nozzles and additive injection valves support eco-friendly Warm Mix Asphalt production, lowering mixing temperatures by 30-50°F and significantly reducing greenhouse gas emissions during urban utility repaving.
As a global leader in industrial mixing machinery operating 3 dedicated production bases spanning 30,000 square meters in Qingdao, China, CO-NELE combines high-precision heavy engineering with uncompromised component sourcing. We bridge the gap between competitive direct-factory pricing and US-grade operational reliability.
Our gearboxes and mixing shafts are fully machined in-house using heavy-duty CNC boring centers. Dynamic load testing and ultrasonic weld flaw inspection ensure uninterrupted performance under 24/7 continuous quarry operating conditions.
Every mixer destined for the North American market features NEMA 4X weather-proof enclosures, UL 508A compliant control panels, premium SEW-Eurodrive or Nord gearmotors, and Allen-Bradley / Siemens PLC controls.
We maintain standardized bolt-on wear liner kits, mechanical shaft seals, and spare mixing arms. Rapid air freight dispatch guarantees wear part deliveries to North American job sites within 48 to 72 hours.
The asphalt industry in North America is undergoing a technological transformation aimed at reducing carbon intensity while lowering lifecycle cost per ton of produced mix. Key industry vectors driving mixing equipment selection include:
By directly injecting micro-foamed bitumen into the twin shaft chamber, asphalt viscosity is reduced without high aggregate heating temperatures. This technology decreases fuel consumption by up to 20% and lowers emissions at the batch facility.
As virgin aggregate and binder prices escalate, mixing high ratios of reclaimed asphalt pavement (RAP) becomes paramount. Twin shaft mixers eliminate cold-spot thermal shocks, evenly re-activating aged bitumen coatings without damaging virgin binders.
Equipped with automated multi-channel grease lubrication systems and digital pressure sensors, CO-NELE mixers automatically purge contamination from shaft end seals, feeding real-time diagnostic telemetry to plant SCADA systems.
To accommodate mobile highway contractors and temporary asphalt production sites, our mixers are designed with compact skid frames, allowing quick containerized transport and plug-and-play installation within 48 hours.
In-depth answers curated by CO-NELE asphalt equipment process engineers for US project managers, EPC contractors, and asphalt plant operators.
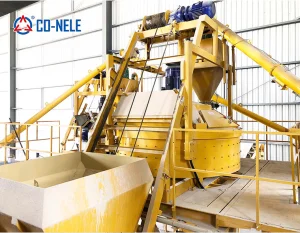
Explore our comprehensive industrial product line, engineered to serve concrete paving, refractory, battery materials, and heavy civil construction projects nationwide.
Partner directly with Qingdao CO-NELE Machinery Co., Ltd.—China's premier manufacturer of high-performance mixing equipment serving contractors across North America. Receive tailored engineering drawings, capacity calculations, and factory-direct pricing.
Send Inquiry Now