
CO-NELEMixing & Granulation
Engineered to deliver strict coefficient of variation (CV < 3%), extreme frost resistance, and high-frequency discharge cycles for automated block manufacturing lines.
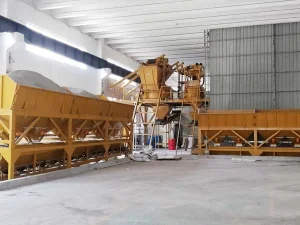
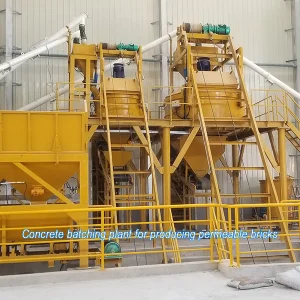
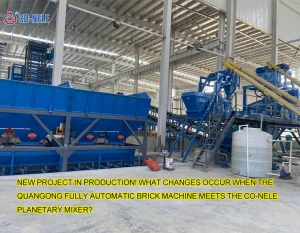
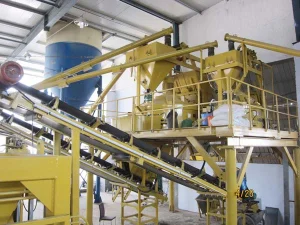
Understanding the severe climatic conditions, urban renewal mandates, and GOST compliance demands shaping concrete block manufacturing in Moscow and the wider Central Federal District.
The city of Moscow is currently experiencing one of the most comprehensive urban modernization drives in Eastern Europe. Driven by the massive Moscow Housing Renovatsiya Programme, the extension of the Moscow Metro network, and major logistics corridor developments around the Central Ring Road (CKAD), demand for high-grade precast concrete blocks, paving stones, foundation blocks (FBS), and kerb units has reached unprecedented levels.
However, supplying concrete blocks to the Moscow market requires stringent adherence to Russian state standards (GOST 26633-2015 for heavy concrete and GOST 17608-2017 for concrete paving plates). Due to Moscow's harsh continental climate—characterized by freezing winter temperatures dipping down to -30°C and frequent freeze-thaw cycles in autumn and spring—concrete blocks produced for municipal and residential use must achieve exceptional density, low water absorption (< 5%), and a frost-resistance rating of F200 to F400.
Standard concrete batching plants designed for temperate zones fail rapidly in Moscow's winter ecosystem. Concrete block manufacturing factories operating around Moscow require specialized thermal insulation, automated steam injection, and rapid aggregate heating systems. CO-NELE batching plants custom-engineered for Moscow incorporate double-layer sandwich panel enclosures, automatic aggregate bin covers, and high-pressure steam distribution manifolds to maintain batch temperatures at a consistent +15°C to +20°C even when raw sand and gravel are loaded at frozen ambient temperatures.
Furthermore, dry-cast concrete block recipes rely heavily on zero-slump or semi-dry concrete mix designs. Achieving instantaneous water activation and homogeneous dispersion of chemical additives (such as air-entraining agents and anti-freezing admixtures) requires high-shear forced-action mixing rather than conventional gravity twin-shaft agitation.
In recent years, the economic and logistical environment for Moscow concrete producers has shifted dramatically. Legacy European machinery manufacturers often present inflated capital expenditure (CAPEX) hurdles, prolonged delivery timelines exceeding 10 to 12 months, and increasingly restricted access to critical spare parts and PLC firmware updates.
As a result, leading precast block producers in Moscow Oblast are actively transitioning to premier Chinese batching plant engineering factories such as CO-NELE. By offering fully compliant EAC (Eurasian Conformity) certified batching plants equipped with in-house manufactured planetary gearboxes, heavy-duty wear components, and Siemens open-architecture automation, Chinese suppliers deliver a 40% to 60% Total Cost of Ownership (TCO) advantage without sacrificing mixing homogeneity or machine longevity.
Why vertical-shaft counter-current planetary mixers have become the definitive global standard for high-performance dry-cast block and paver batching lines.
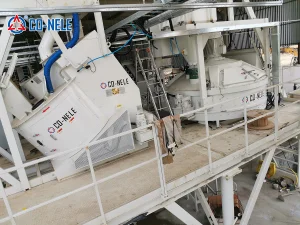
The mixing star rotates on a central vertical axis while simultaneously orbiting around the pan center. This eliminates dead zones and guarantees complete micro-homogeneity within 45 to 60 seconds.
Semi-dry block mixes (w/c ratio 0.26–0.32) require intense mechanical shear to break cement agglomerates. Planetary arms force uniform water film coating on aggregate particles.
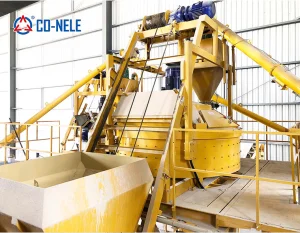
Integrated pneumatic and hydraulic discharge doors sync seamlessly with automatic block molding machines (Masa, Hess, Zenith, Poyatos) for continuous high-speed production.
When producing high-density concrete paving blocks, permeable bricks, and architectural masonry, machine selection dictates product rejection rates and cement consumption. Below is an engineering benchmark comparison:
| Performance Indicator | Vertical Shaft Planetary Mixer (CO-NELE CMP) | Twin-Shaft Compulsory Mixer | Traditional Ring Pan Mixer |
|---|---|---|---|
| Primary Application Target | Dry-cast blocks, pavers, UHPC, color face mix | Ready-mix wet concrete, bulk foundation slabs | Standard masonry mortar, low-spec blocks |
| Mixing Homogeneity (CV) | < 3.0% (Micro-homogeneous) | 5.0% - 8.0% (Macro-homogeneous) | > 8.0% (Risk of cement pockets) |
| Mixing Cycle Time (Dry-Cast) | 45 - 60 seconds | 75 - 90 seconds | 90 - 120 seconds |
| Pigment / Color Dispersion | Instantaneous & Uniform (Zero streak) | Moderate (Requires extra mixing time) | Poor (High risk of color variation) |
| Cement Savings Potential | 5% - 8% Reduction for same strength | Baseline standard | Requires 3-5% extra cement buffer |
| Wear Liner Life (Batches) | 100,000 - 150,000 batches | 60,000 - 80,000 batches | 40,000 - 50,000 batches |
Combining complete vertical integration, rigorous in-house metallurgical testing, and agile manufacturing modularity to serve international industrial procurement goals.
Unlike conventional assembly factories that purchase commercial off-the-shelf industrial gearboxes, CO-NELE designs, machines, and tests its proprietary planetary reducers specifically for severe zero-slump concrete shock loads. Operating across three modern production bases in Qingdao covering 30,000 m², our CNC gear-hobbing and heat-treatment processes guarantee maximum torque transfer, zero oil leakage, and ultra-quiet mechanical operation even under continuous 24/7 block manufacturing schedules.
Concrete block batching involves highly abrasive aggregates, including crushed granite, quartz sand, expanded clay (keramzit), and recycled concrete slag. CO-NELE batching plants utilize replaceable high-chrome cast alloy wear tiles (hardness > 60 HRC) arranged in a specialized rhombus pattern. This design prevents channel gouging and extends wear liner life beyond 120,000 batches, drastically lowering routine maintenance downtime for Moscow plant owners.
China’s mature industrial infrastructure allows CO-NELE to procure high-grade structural steel, premium pneumatic components (Festo/AirTAC), and electrical systems (Siemens/Schneider) at optimized cost scales. We pass these savings directly to our customers, allowing a Moscow block manufacturer to acquire a complete, winterized, automated planetary batching plant line for a fraction of the cost of European equivalents while maintaining superior batch accuracy.
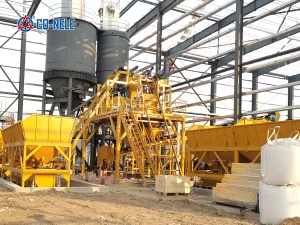
Time-to-market is crucial during short high-season construction windows in Northern latitudes. CO-NELE designs modular containerized batching plants that are pre-assembled, pre-wired, and fully tested in our factory prior to shipment. Standard block batching plants can be shipped to Moscow via direct rail freight or sea-to-rail routes within 35 to 45 days, followed by rapid 7-day on-site mechanical erection.
Tailored mixing and batching configurations meeting specialized structural, environmental, and aesthetic requirements of urban developments.
Moscow municipal pavement upgrade projects require double-layer interlocking pavers. Our batching plant systems can be configured with twin planetary mixers: a larger CMP unit supplying high-strength coarse aggregate base concrete, and a smaller CMP unit delivering ultra-precise, color-pigmented fine aggregate face mix with zero color bleed.
Kerb stones installed along Moscow highways (MKAD) must withstand heavy mechanical impacts from snowplows and de-icing chemicals (sodium chloride, calcium chloride). CO-NELE batching plants formulate dense, zero-slump concrete with precise air-entrainment dosing, ensuring compliance with rigorous freeze-thaw standards.
To prevent urban flooding in Moscow's expanding suburban districts, permeable paving bricks with porous aggregate matrices are heavily specified. The CMP planetary batching plant handles coarse aggregate gravel without crushing particle fractions, maintaining optimal void ratios while guaranteeing cement-paste wrapping.
For energy-efficient wall construction in residential complexes around Moscow, lightweight aggregate concrete (expanded clay / keramzit) is widely utilized. CO-NELE planetary mixers gentle-action kinematics prevent aggregate floatation and particle degradation, producing homogenous lightweight thermal blocks.
How CO-NELE fulfills international tender specifications, quality assurance protocols, and automated plant governance for institutional buyers.
International procurement directors operating across Eurasia require robust legal and engineering compliance before authorizing equipment purchases. All CO-NELE concrete block batching plants and industrial planetary mixers are fully certified under the EAC Technical Regulations (TR CU 010/2011 on Safety of Machinery and Equipment), enabling seamless custom clearance and official industrial operation across Russia, Belarus, Kazakhstan, and Armenia.
In addition, our manufacturing facilities adhere strictly to ISO9001 Quality Management Systems, ISO14001 Environmental Standards, and European CE Directives for electrical and mechanical safety.
Water-cement ratio variation of even 0.5% can cause severe color discrepancies, strength failures, and dimensional deviations in concrete block molding. CO-NELE batching plants feature advanced Siemens PLC automation equipped with high-speed microwave moisture sensors mounted inside aggregate bins and underneath the mixing pan.
The control system reads aggregate moisture content in real-time, automatically calculating dynamic batch adjustments to water and sand dosing within milliseconds. Plant managers in Moscow can track batch reports, aggregate consumption, and remote diagnostic logs via cloud telemetry interfaces.
Direct answers from our senior concrete process engineering team regarding batching plant selection, winter operating conditions, and maintenance protocols.
Explore our comprehensive portfolio of planetary mixers, dry mortar lines, twin-shaft plants, and granulating equipment engineered for global deployment.
Send us your material specifications, required hourly capacity (m³/h), and site constraints. Our senior application engineers will deliver a customized technical proposal, plant CAD drawing, and competitive quotation within 24 hours.
Send Inquiry Now