
CO-NELEMixing & Granulation
Specifically matched to the high-ambient thermal demands, rapid relocation needs, and dense footprint limitations of infrastructure projects across Riyadh and the Central Province.
Analyzing the structural shifts, urban density challenges, and equipment standards required for the Middle East's fastest-growing metropolis.
The transformation of Riyadh—driven by landmark developments such as New Murabba, King Salman Park, Diriyah Gate, and the expansion of the King Khalid International Airport corridor—has generated unprecedented demand for structural concrete. However, urban density and strict municipal logistics rules limit traditional, expansive ready-mix plants within city boundaries.
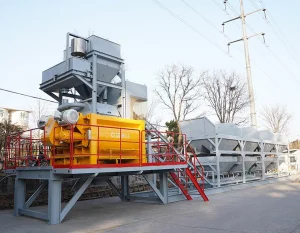
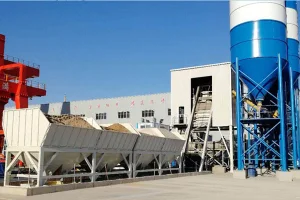
Compact concrete batching plants have emerged as the primary strategic equipment asset for main contractors in Riyadh. Delivering outputs from 25 m³/h to 90 m³/h on minimal footprints (often under 250 m²), these plants allow contractors to set up directly on construction sites, bypassing urban transit delays and slump loss caused by traffic congestion on major arteries like King Fahd Road and Northern Ring Road.
Summer operating conditions in Riyadh frequently exceed 45°C to 50°C, creating severe challenges for hydration control, slump retention, and compressive strength development. Standard concrete mixing units fail to maintain batch temperatures below the 32°C threshold mandated by Saudi Building Code (SBC 304).
CO-NELE compact batching plants integrated for the Riyadh market feature engineered thermal protection: heat-insulated aggregate storage bins, twin-chilled water dosing systems, integrated flaked-ice dosing screw chutes, and high-speed forced-action planetary mixing pan linings. This enables precise temperature management even under peak summer radiant heat.
Data compiled from over 45 installation sites across Riyadh's Industrial Cities (MODON Phase 1, 2, and 3) highlights the efficiency advantages of modern compact modular plants versus legacy stationary layouts.
Why vertical-shaft counter-current mixing outperforms traditional tilt-drum and standard twin-shaft systems in high-performance Saudi applications.
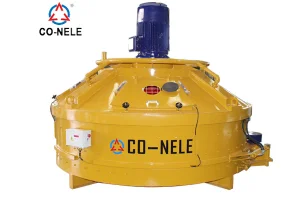
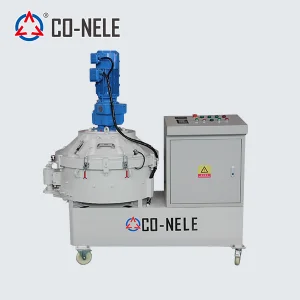
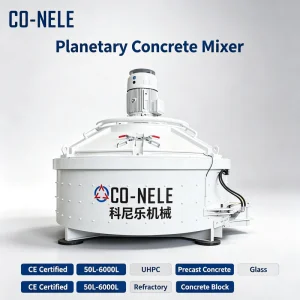
CO-NELE CMP series planetary concrete mixers utilize complex revolution and rotation trajectories. The mixing arms revolve clockwise while rotating counter-clockwise around the central axis. This counter-current movement ensures 100% pan coverage with zero dead angles, achieving micro-dispersion of micro-silica, fly ash, and chemical admixtures within 45 to 60 seconds.
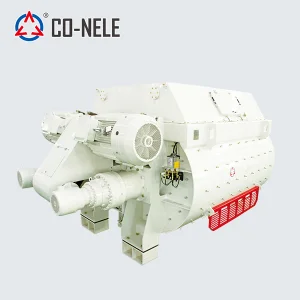
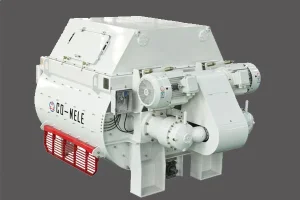
Unlike competitors who assemble third-party gearboxes, CO-NELE designs and manufactures parallel-shaft planetary gearboxes specifically for high-resistance concrete mixes (UHPC, dry-cast, and heavy aggregate recipes). Featuring hardened alloy gears and mechanical seal systems, these reducers deliver uninterrupted torque transmission under heavy thermal load.
Crushed desert sand and granite aggregates in the Riyadh region present high silica abrasiveness. CO-NELE mixing pans are lined with replaceable high-chrome cast alloy liners (HB600+) and wear-resistant mixing blades (Ni-Hard cast irons), extending wear component lifespans to over 120,000 continuous batch cycles under rigorous field tests.
| Performance Parameter | CO-NELE CMP Compact Planetary Plant | Standard Twin-Shaft Compact Plant | Conventional Stationary Drum Plant |
|---|---|---|---|
| Concrete Homogeneity (CV%) | < 3.0% (Micro-level uniformity) | 5.0% - 7.0% (Standard concrete) | > 10.0% (High variation) |
| Mixing Time (C50/60 High-Strength) | 35 - 45 Seconds | 60 - 75 Seconds | 90 - 120 Seconds |
| Ultra-High Performance Concrete (UHPC) | Fully Capable (Dedicated Configuration) | Limited / Requires Modified Motors | Not Suitable |
| Riyadh Foundation / Installation Time | 3 Days (Steel chassis base) | 5 - 7 Days (Semi-foundation) | 21 - 30 Days (Heavy concrete pit) |
| Water & Dust Pollution Control | Enclosed Pulsed Jet Baghouse Filters | Standard Water Spray / Basic Filter | Open Discharge / High Dust |
Turnkey plant configurations tailored to Saudi Arabian Standards Organization (SASO), Ministry of Transport (MOT), and Aramco specification benchmarks.
Modern Saudi infrastructure contracts mandate digital traceable batch records. CO-NELE compact plants integrated for Riyadh feature Siemens S7 PLC controllers with multi-language (Arabic/English) SCADA touch-panel interfaces. Real-time batching accuracy for cement, silica fume, water, and chemical admixtures is maintained within ±1%, backed by high-precision load cells and dynamic weight compensation algorithms.
Microwave moisture sensor systems (Hydronix integration option) continuously measure fine aggregate moisture in aggregate bins, automatically adjusting water addition in real time to guarantee precise water-cement ratios (w/c) essential for hot-weather casting.
Water management is critical in Riyadh's arid climate. CO-NELE integrated batching solutions incorporate closed-loop wash-out reclaimer systems. Alkaline mixer wash water is filtered and recycled directly into non-structural concrete batches or dust suppression systems, achieving 0% liquid waste discharge and complying with Saudi National Environmental Compliance Center (NCEC) mandates.
Deploying equipment in Riyadh requires immediate technical response to avoid project downtime. CO-NELE supports client operations across the Kingdom through dedicated field engineering teams and local spare parts inventory hubs:
Addressing key engineering, procurement, and operational inquiries from Saudi contractors and project managers.
Vertical-shaft planetary mixers use a counter-current mixing action that eliminates unmixed pockets, ensuring consistent dispersion of fine pigments, silica fume, and micro-fibers. For precast elements (such as kerb stones, boundary walls, and prestressed beams) produced under hot arid conditions, planetary mixers guarantee low water-cement ratio consistency, reducing surface honeycombing and ensuring compliance with SASO tensile and compressive standards.
CO-NELE Riyadh-edition compact plants feature modular thermal engineering, including thermal insulation jackets on water tanks, dedicated ice-weighing hoppers with screw feeders, covered aggregate bin canopies with automatic water misting, and continuous moisture/temperature probe integration in the mixer pan. This ensures fresh concrete temperatures remain strictly within SBC 304 limits (< 32°C).
CO-NELE compact plants are designed on heavy-duty structural steel base frames. They require only a leveled, reinforced concrete slab (typically 20-25 cm thick depending on soil bearing capacity) rather than deep subterranean pits or complex foundation footings. This cuts civil works preparation costs by up to 70% and enables plant relocation in under 3 days.
CO-NELE maintains standard modular components in stock. Manufacturing takes 20 to 30 days. Shipping from Qingdao Port to Jeddah Islamic Port or Dammam Port takes approximately 22 to 28 days. All equipment is fully pre-registered on the Saudi SABER e-platform, issued with Certificates of Conformity (CoC), and meets SASO low-voltage and machinery safety directives for immediate customs clearance.
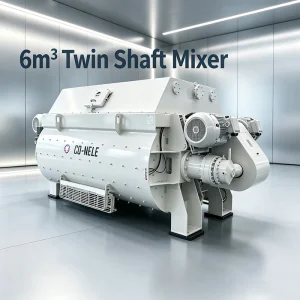
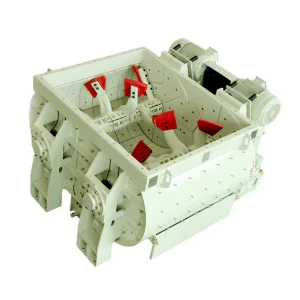
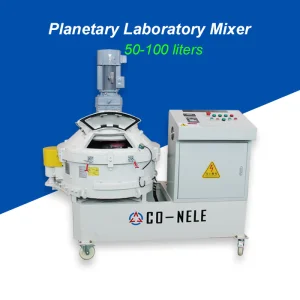
Explore specialized laboratory mixers, high-intensity industrial granulators, UHPC mixing plants, and heavy-duty shaft mixers deployed worldwide.
Consult with CO-NELE Senior Process Engineers. Receive detailed plant CAD drawings, site footprint analyses, SASO compliance documentation, and factory-direct pricing within 24 hours.