
CO-NELEMixing & Granulation
Engineered for maximum compressive strength, low water-cement ratios, and zero binder waste. Powered by CO-NELE counter-current mixing kinematics.
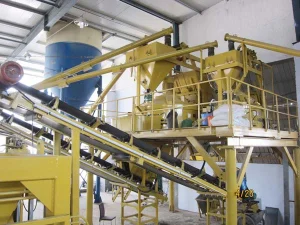
Vertical-shaft forced mixing delivering under 3% coefficient of variation for high-density architectural masonry units.
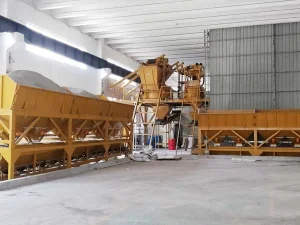
Heavy-duty planetary mixing system optimized for fine aggregates, manufactured sand, and rapid pigments distribution.
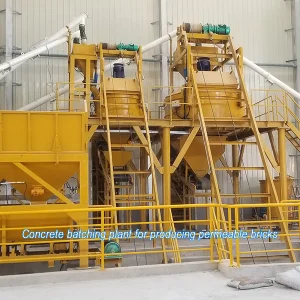
Turnkey batching plant optimized for eco-friendly pervious concrete blocks and urban drainage paving systems.
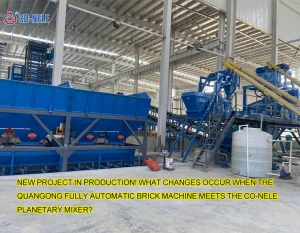
Dual-feed automated aggregate batching system engineered for high-volume commercial paver production.
The Greater Sydney region is undergoing an unprecedented infrastructure boom. Key projects such as the Western Sydney Aerotropolis, Sydney Metro West, the M12 Motorway, and extensive commercial logistics hubs across Western Sydney (Parramatta, Badgerys Creek, Kemps Creek, and Penrith) have escalated the demand for structural masonry, heavy-duty retaining wall blocks, and interlock paving units.
To meet Transport for NSW (TfNSW) specifications and civil engineering standards, local block factories require batching plants capable of producing concrete mixes with ultra-consistent water-cement ratios and high early strength development.
Sydney’s aggregate supply relies heavily on crushed river gravel, Hawkesbury sandstone manufactured sand (M-Sand), and basalt quarry screenings from the Illawarra and Hunter regions. Natural sand scarcity has forced Sydney producers to pivot toward manufactured aggregates, which exhibit higher angularity, variable moisture absorption, and fine-particle content.
Standard twin-shaft or pan mixers often struggle with shear distribution in dry-cast block mixtures using high-percentage manufactured sand, resulting in edge crumbling and density variance. CO-NELE’s planetary counter-current mixing technology overcomes this by providing intense mechanical shear, guaranteeing uniform cement paste coating over every aggregate particle.
From port facilities to suburban housing estates, modern concrete block batching plants in Sydney must handle a diverse spectrum of specialized mix designs.
Used extensively at Port Botany Container Terminals, intermodal freight hubs, and industrial warehousing in outer Sydney. These blocks require C50/60 concrete strength, high abrasion resistance, and extreme resistance to wheel loads up to 100 tonnes. Our batching plants ensure exact aggregate grading and moisture dosing for dense dry-cast compression.
Water Sensitive Urban Design (WSUD) regulations mandated by local councils across Greater Sydney require permeable paving solutions to mitigate stormwater runoff. Producing zero-slump permeable concrete demands zero segregation during mixing—a feat natively achieved by CO-NELE’s planetary mixers without cement balling.
For high-end residential estates in the Northern Beaches, Hills District, and South Sydney, colored face blocks and split-face retaining wall units require absolute batch-to-batch color repeatability. Our planetary mixing system distributes iron oxide pigments uniformly within 45 to 60 seconds.
Understanding the physics of forced high-shear batching for ultra-low slump, dry-cast, and binder-reduced concrete mixes.
Unlike standard ready-mix concrete which flows easily at slumps of 80mm to 120mm, concrete used in automatic block-making machines (such as Hess, Masa, Zenith, or Columbia block machines) is dry-cast (zero slump) with water-cement ratios frequently below 0.32. Under these dry conditions, traditional twin-shaft mixers suffer from severe dead-zone formation, high blade drag, and uneven moisture distribution.
CO-NELE’s vertical-shaft planetary mixers utilize a synchronized counter-current mixing movement. The mixing arms rotate on a central vertical axis while simultaneously orbiting along a planetary trajectory. This mechanical path ensures that 100% of the pan floor is swept twice per revolution, leaving no dead angles and achieving complete micro-homogeneity within 60 seconds.
| Mixer Specification & Performance Metric | CO-NELE Planetary Counter-Current | Traditional Twin-Shaft Mixer | Standard Vertical Pan Mixer |
|---|---|---|---|
| Mixing Kinematics | Synchronized Rotation + Revolution | Dual Horizontal Axis Parallel Rotation | Fixed Single Axis Center Rotation |
| Mix Homogeneity (Coefficient of Variation) | < 3.0% (Micro-Homogeneous) | 5.0% - 8.0% (Standard) | > 8.5% (High Variance) |
| Performance on Zero-Slump / Dry-Cast Concrete | Exceptional (No Balling or Clumping) | Moderate (Risk of dead zones) | Poor (High segregation) |
| Pigment Dispersion Time (Iron Oxide) | 45 - 60 Seconds | 90 - 120 Seconds | 120+ Seconds |
| Cement Consumption Efficiency | Optimized (10-15% Savings) | Baseline Standard | High Cement Requirement |
| Energy Consumption per m³ Batch | Low (Direct Planetary Reducer) | Moderate to High | High Drag Losses |
Under NSW EPA regulations and Australian Green Star building codes, concrete producers are under mounting pressure to reduce carbon footprints by substituting Portland cement with Fly Ash (from Eraring & Bayswater power stations) and Ground Granulated Blast Furnace Slag (GGBFS from Port Kembla).
Because SCMs have distinct specific surface areas and hydration kinetics, thorough mechanical shearing is paramount. Our plants feature dynamic microwave moisture probes (Sonoplan / Hydronix compatible) mounted in the pan floor to continuously adjust water batching in real-time, accounting for fine SCM fluctuations.
CO-NELE batching plants delivered to Sydney are equipped with Siemens S7-1500 PLC batching computers and SCADA visualization software. Operators can store over 1,000 distinct concrete recipes, manage inventory, export automated delivery dockets, and perform cloud-based remote diagnostics for zero unscheduled downtime.
Why leading global concrete producers and Sydney operators partner directly with CO-NELE mixing machinery.
Unlike assemblers who buy generic commercial gearboxes, CO-NELE designs and manufactures dedicated vertical planetary reducers in our 30,000 m² Qingdao facility. Engineered specifically to handle shock loads during zero-slump block mixing, our gearboxes undergo strict no-load and full-load test bench trials before shipment.
We supply cast chromium alloy liner plates (hardness ≥62 HRC) and rubber-shielded mixing blades specifically formulated to resist abrasive Sydney aggregate blends (quartz sand, broken basalt). Field records confirm liner longevity exceeding 120,000 to 150,000 continuous block batching cycles.
With direct container shipping routes from Qingdao Port to Sydney (Port Botany), standard batching modules and planetary mixers achieve typical sea transport times of just 14 to 18 days. Pre-assembled modular frames fit seamlessly inside standard 40ft OT or HQ containers to minimize ocean freight costs.
Ensuring complete peace of mind for Australian factory owners, plant managers, and site safety inspectors.
All batching plants and mixers supplied into Australia are custom engineered to satisfy rigorous local regulatory frameworks:
We back our machinery with comprehensive technical support tailored for Sydney operators:
Select the ideal mixing plant layout for your specific output requirements, factory footprint, and block machine integration.
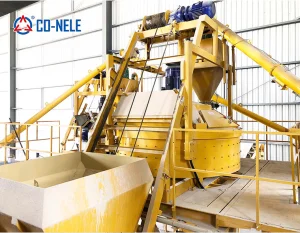
High-capacity plant designed for producing heavy-duty road bricks, concrete kerbs, and drainage channels.
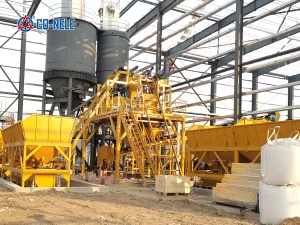
Planetary mixer technology engineered for high-finish road tiles, pavers, and decorative concrete products.
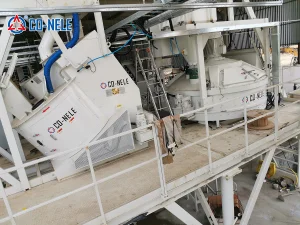
Fully automated batching plant integrated for high-speed hollow block and precast floor slab production lines.
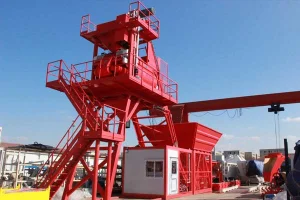
Rapid-deployment mobile batching plant featuring a wheel chassis for quick setup on regional NSW job sites.
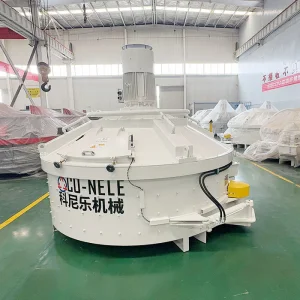
Reinforced high-shear planetary mixer designed for abrasive refractories, UHPC, and high-tech mineral castables.
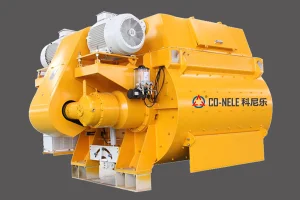
High-output 2.0m³ compacted output twin-shaft mixer with dual hydraulic discharge gates for mass concrete production.
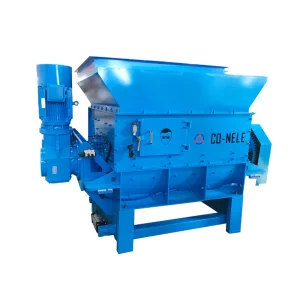
Industrial batch mixing station for cold/hot mix asphalt, tile adhesives, and specialized dry mortar formulations.
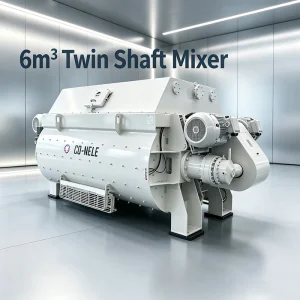
Heavy-duty 6.0m³ batch volume concrete mixer designed for mega ready-mix facilities and dam construction projects.
Technical guidance for plant engineers and investment directors evaluating new concrete batching machinery.
A planetary counter-current mixer is essential for block, paver, and masonry manufacturing because block concrete is dry-cast with a near-zero slump (W/C ratio typically 0.28-0.34). Twin-shaft mixers rely on liquid fluidity to assist mixing motion and often leave dry pockets or aggregate balling in zero-slump mixes. CO-NELE’s planetary mixer mechanically forces 100% of the material through high-shear counter-current star arms, achieving complete cement hydration and pigment coating within 45 to 60 seconds.
Every plant destined for New South Wales or Australia is customized at our factory with 415V, 50Hz 3-Phase power configurations. Control panels are built using CE / UL / RCM compliant components (Siemens PLC, Schneider breakers, IP65 enclosures), dual-channel emergency stop circuits, safety door interlocks compliant with AS 4024, and standardized wiring schematics provided in English.
Yes. Manufactured sand exhibits high angularity and varying micro-fines, which increases water demand and wear rate on mixer liners. CO-NELE batching plants utilize high-chrome alloy wear plates (hardness ≥ 62 HRC) and optional floor-mounted microwave moisture sensors that continuously adjust batching water volume to maintain consistent concrete workability regardless of aggregate moisture fluctuations.
Manufacturing lead time is typically 30 to 40 days depending on plant customization. Ocean transit from Qingdao Port to Port Botany (Sydney) takes approximately 14 to 18 days. Modular foundationless or compact plants can be fully assembled, wired, and wet-tested on site in Sydney within 7 to 10 days by local mechanical contractors under remote or on-site supervision from CO-NELE engineers.
By partnering directly with CO-NELE (the original manufacturer with 80+ patents and 3 production bases), Sydney buyers eliminate middleman distributor markups of 30-50%. You receive factory-direct technical engineering, direct access to spare parts at cost, and custom modular engineering tailored precisely to your factory building height and block machine feed belt layout.
Request a custom technical proposal, plant CAD layout drawing, and factory-direct quotation within 24 hours. Speak directly with our mixing process engineers.